




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Can Your Existing Cartoner Work with a Wafer Packaging Line?
In most cases, a wafer packaging system can be integrated with an existing cartoner, provided the packaged product, transfer layout, production rate, and control interfaces are compatible. The line can be designed to move sealed wafer packs continuously from a horizontal flow wrapper to downstream cartoning equipment. Before the final design is approved, the actual wafer samples, packaging film, carton format, and cartoner specifications should be evaluated together.
Integration Overview
The connection point is normally the discharge section of the horizontal flow packaging machine. Once wafers are fed, aligned, wrapped, sealed, and cut, the finished packs are transferred toward the cartoner through a conveyor or synchronized infeed device. The discharge pattern must match the cartoner's required product direction, spacing, and loading arrangement.
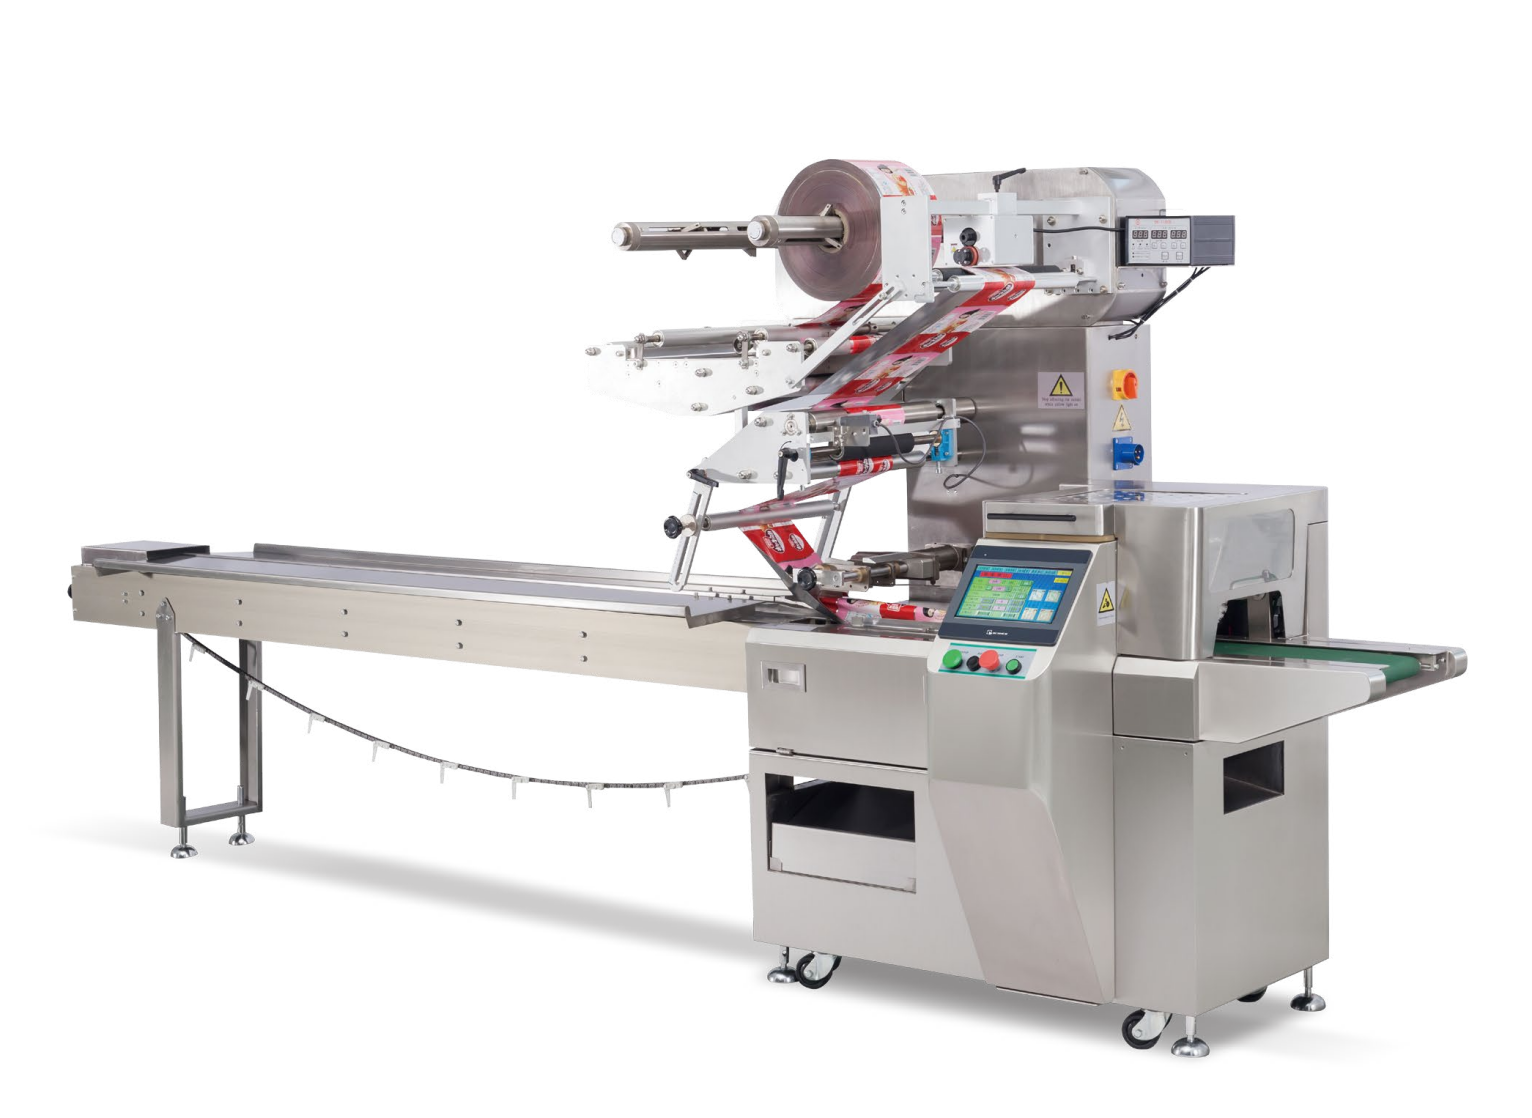
A high-speed cartoner is available as an optional downstream module for the wafer automatic packaging system. This makes it possible to configure a complete primary and secondary packaging line, although an existing cartoner cannot be assumed to be compatible without a technical review.
What Must Be Checked Before Connection?
Pack Size and Loading Pattern
The wrapped wafer pack must fall within the cartoner's accepted product envelope. The listed finished-pack dimensions are generally about 60–300 mm in length, 35–200 mm in width, and 5–120 mm in height, depending on the model and product. The cartoner should also be checked for its required pack orientation, pack quantity per carton, loading sequence, and permissible product spacing.
Conveyor Transfer and Product Orientation
The wafer line can include belt conveyors with side guides, vibratory alignment tracks, photoelectric sensors, stacking devices, and collating functions. These components help create a stable, evenly spaced product stream for the cartoner. Optional stacking can arrange two to six wafers per pack, while the final orientation and grouping must correspond to the cartoner's infeed design.
Throughput and Synchronization
The flow wrapper and cartoner need to operate at compatible speeds. The transfer section may require buffering, servo synchronization, or a customized conveyor layout to prevent pack accumulation and maintain consistent carton loading. The required operating rate, pack spacing, changeover requirements, and available installation area should be confirmed during line engineering.
Controls and Communication
The packaging system uses PLC-based control with distributed servo drives. Its control functions can include a color touchscreen, recipe storage, fault records, remote access, and EtherCAT or CANopen communication options. If the current cartoner uses another control architecture, the signal exchange, safety circuits, start-stop logic, alarms, and handshake requirements must be defined in advance. There is no single plug-and-play protocol guaranteed for every cartoner model.
Packaging Process and Equipment Arrangement
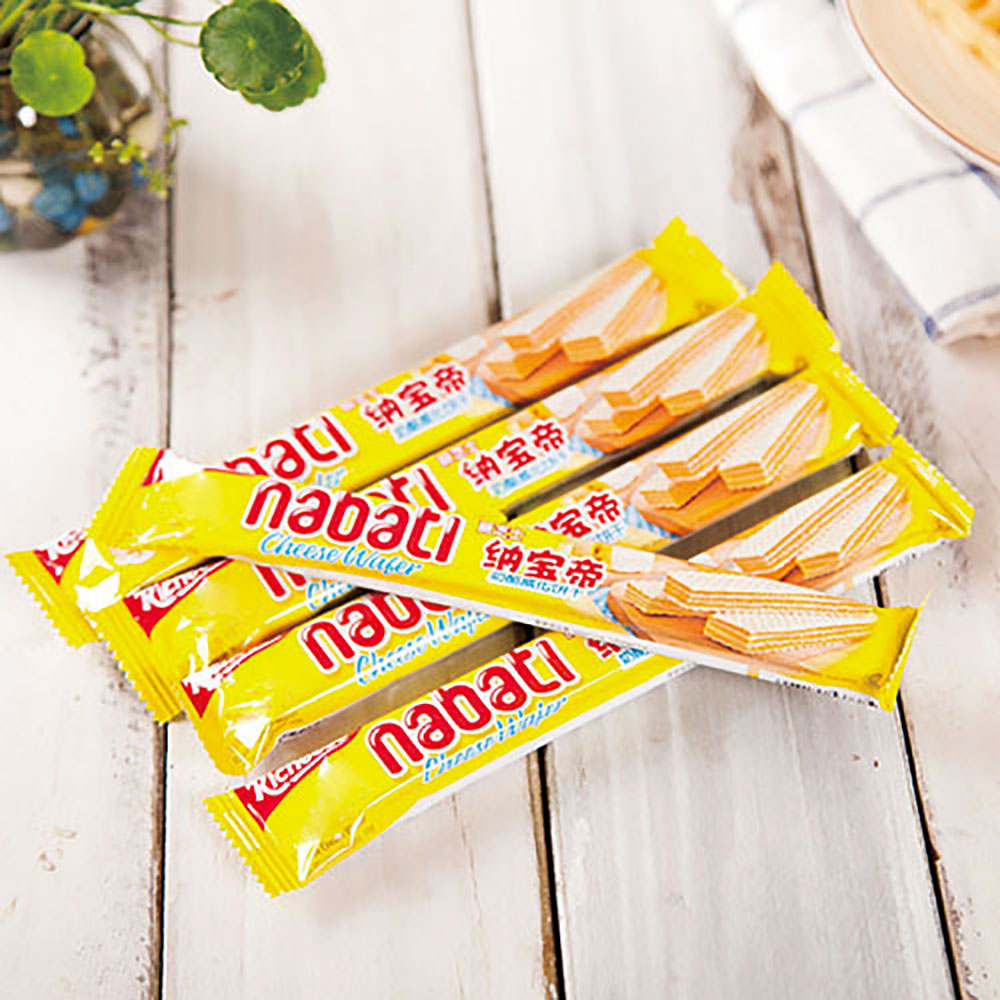
The system uses horizontal flow wrapping for wafer biscuits, wafer bars, creamed wafers, sandwich wafers, and chocolate-coated wafers. Product feeding and alignment take place before the film is formed around the wafer. The machine then creates a longitudinal fin seal, applies heated end seals, cuts the film, and discharges the completed pillow packs. From there, the packs can be aligned, stacked, collated, and sent to a cartoner for secondary packaging.
This architecture is suitable for production lines in which individually wrapped wafers must move directly into cartons without manual handling. The exact feeder, collator, transfer conveyor, and cartoner interface depend on the wafer dimensions, product grouping, carton design, and target output.
Compatibility Information to Prepare
To assess an existing cartoner, the following information should be supplied:
- Cartoner manufacturer and model
- Pack length, width, height, weight, and orientation
- Required packs per carton and carton loading pattern
- Cartoner speed and permitted infeed spacing
- Carton dimensions and changeover range
- Available conveyor length and transfer direction
- PLC, communication, safety, and signal interface details
- Wafer samples, film specifications, and finished-pack samples
Recommended Validation Procedure
Sample testing should be completed before the equipment configuration is finalized. A practical trial should use the customer's actual wafers, film, pack dimensions, and cartons. It should verify product feeding, seal quality, discharge stability, pack orientation, conveyor transfer, carton loading, rejected-product handling, speed coordination, and recipe changeover.
Ruipuhua has experience developing connected packaging solutions for bakery products, biscuits, wafers, snacks, noodles, and related food products. Its engineering scope includes feeding, horizontal form-fill-seal packaging, secondary collating, case packing, and robotic palletizing. A documented chocolate pie cake project for Orion plants in China included wrapping and robotic palletizing, demonstrating experience with integrated packaging lines. However, the compatibility of a particular existing cartoner still requires project-specific testing.
Integration Capability at a Glance
| Integration factor | Available solution or requirement |
|---|---|
| Primary packaging method | Horizontal pillow packaging with longitudinal fin seals and heated cross seals |
| Cartoner connection | High-speed cartoner available as an optional downstream module |
| Finished-pack dimensions | Typical range of 60–300 mm length, 35–200 mm width, and 5–120 mm height, subject to model and product |
| Product transfer | Continuous discharge with optional alignment, stacking, and collating |
| Control system | PLC control, servo drives, recipe management, diagnostics, and optional EtherCAT or CANopen communication |
| Pre-delivery verification | Testing with customer products, film, packs, and cartons |
Frequently Asked Questions
Will the wafer line connect directly to any cartoner?
No. The connection must be engineered around the cartoner's mechanical infeed, acceptable pack range, operating speed, orientation, safety system, and control communication. A technical review is required for each cartoner model.
Can several wafers be grouped before cartoning?
Yes. Depending on the product and configuration, the feeding system can stack two to six wafers per pack and provide collating functions. The selected grouping must match the carton loading pattern and the cartoner's infeed capacity.
What is the best way to confirm compatibility?
Send the cartoner specifications together with wafer samples, film details, target pack dimensions, production speed, and carton samples. A factory trial can then confirm the mechanical transfer, control signals, product handling, and final carton loading performance.
Conclusion
A wafer packaging system can be connected to current cartoning equipment when the pack format, discharge arrangement, throughput, conveyor transfer, and control interfaces are aligned. The optional high-speed cartoner, flexible feeding functions, PLC-based controls, and sample testing process provide a practical foundation for this type of integration. Ruipuhua supplies packaging machinery as an OEM manufacturer, supports orders from one machine, and provides engineering and after-sales assistance. Its listed CE certification covers flow packaging machines, automatic packaging systems, cartoners, and palletizing robots. For technical evaluation or integration support, contact lotuspack@ruipuhua.com.
About Us
Foshan Ruipuhua Machinery Equipment Co. Ltd, also known as RPH or RAPIDPACK, is a Chinese manufacturer of automatic packaging machinery that integrates R&D, production, installation, and technical after-sales service. Established in 2005, the company operates a 50,000-square-meter facility and supplies packaging equipment to more than 100 countries. Its product range includes wafer production and packaging lines, automatic feeding and collating lines, cartoning machines, case packing systems, and palletizing robots. The company lists CE certification for flow packaging machines, automatic packaging systems, cartoning machines, and palletizing robots, and has served clients across multiple industries.
REPORT