




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Power Tools
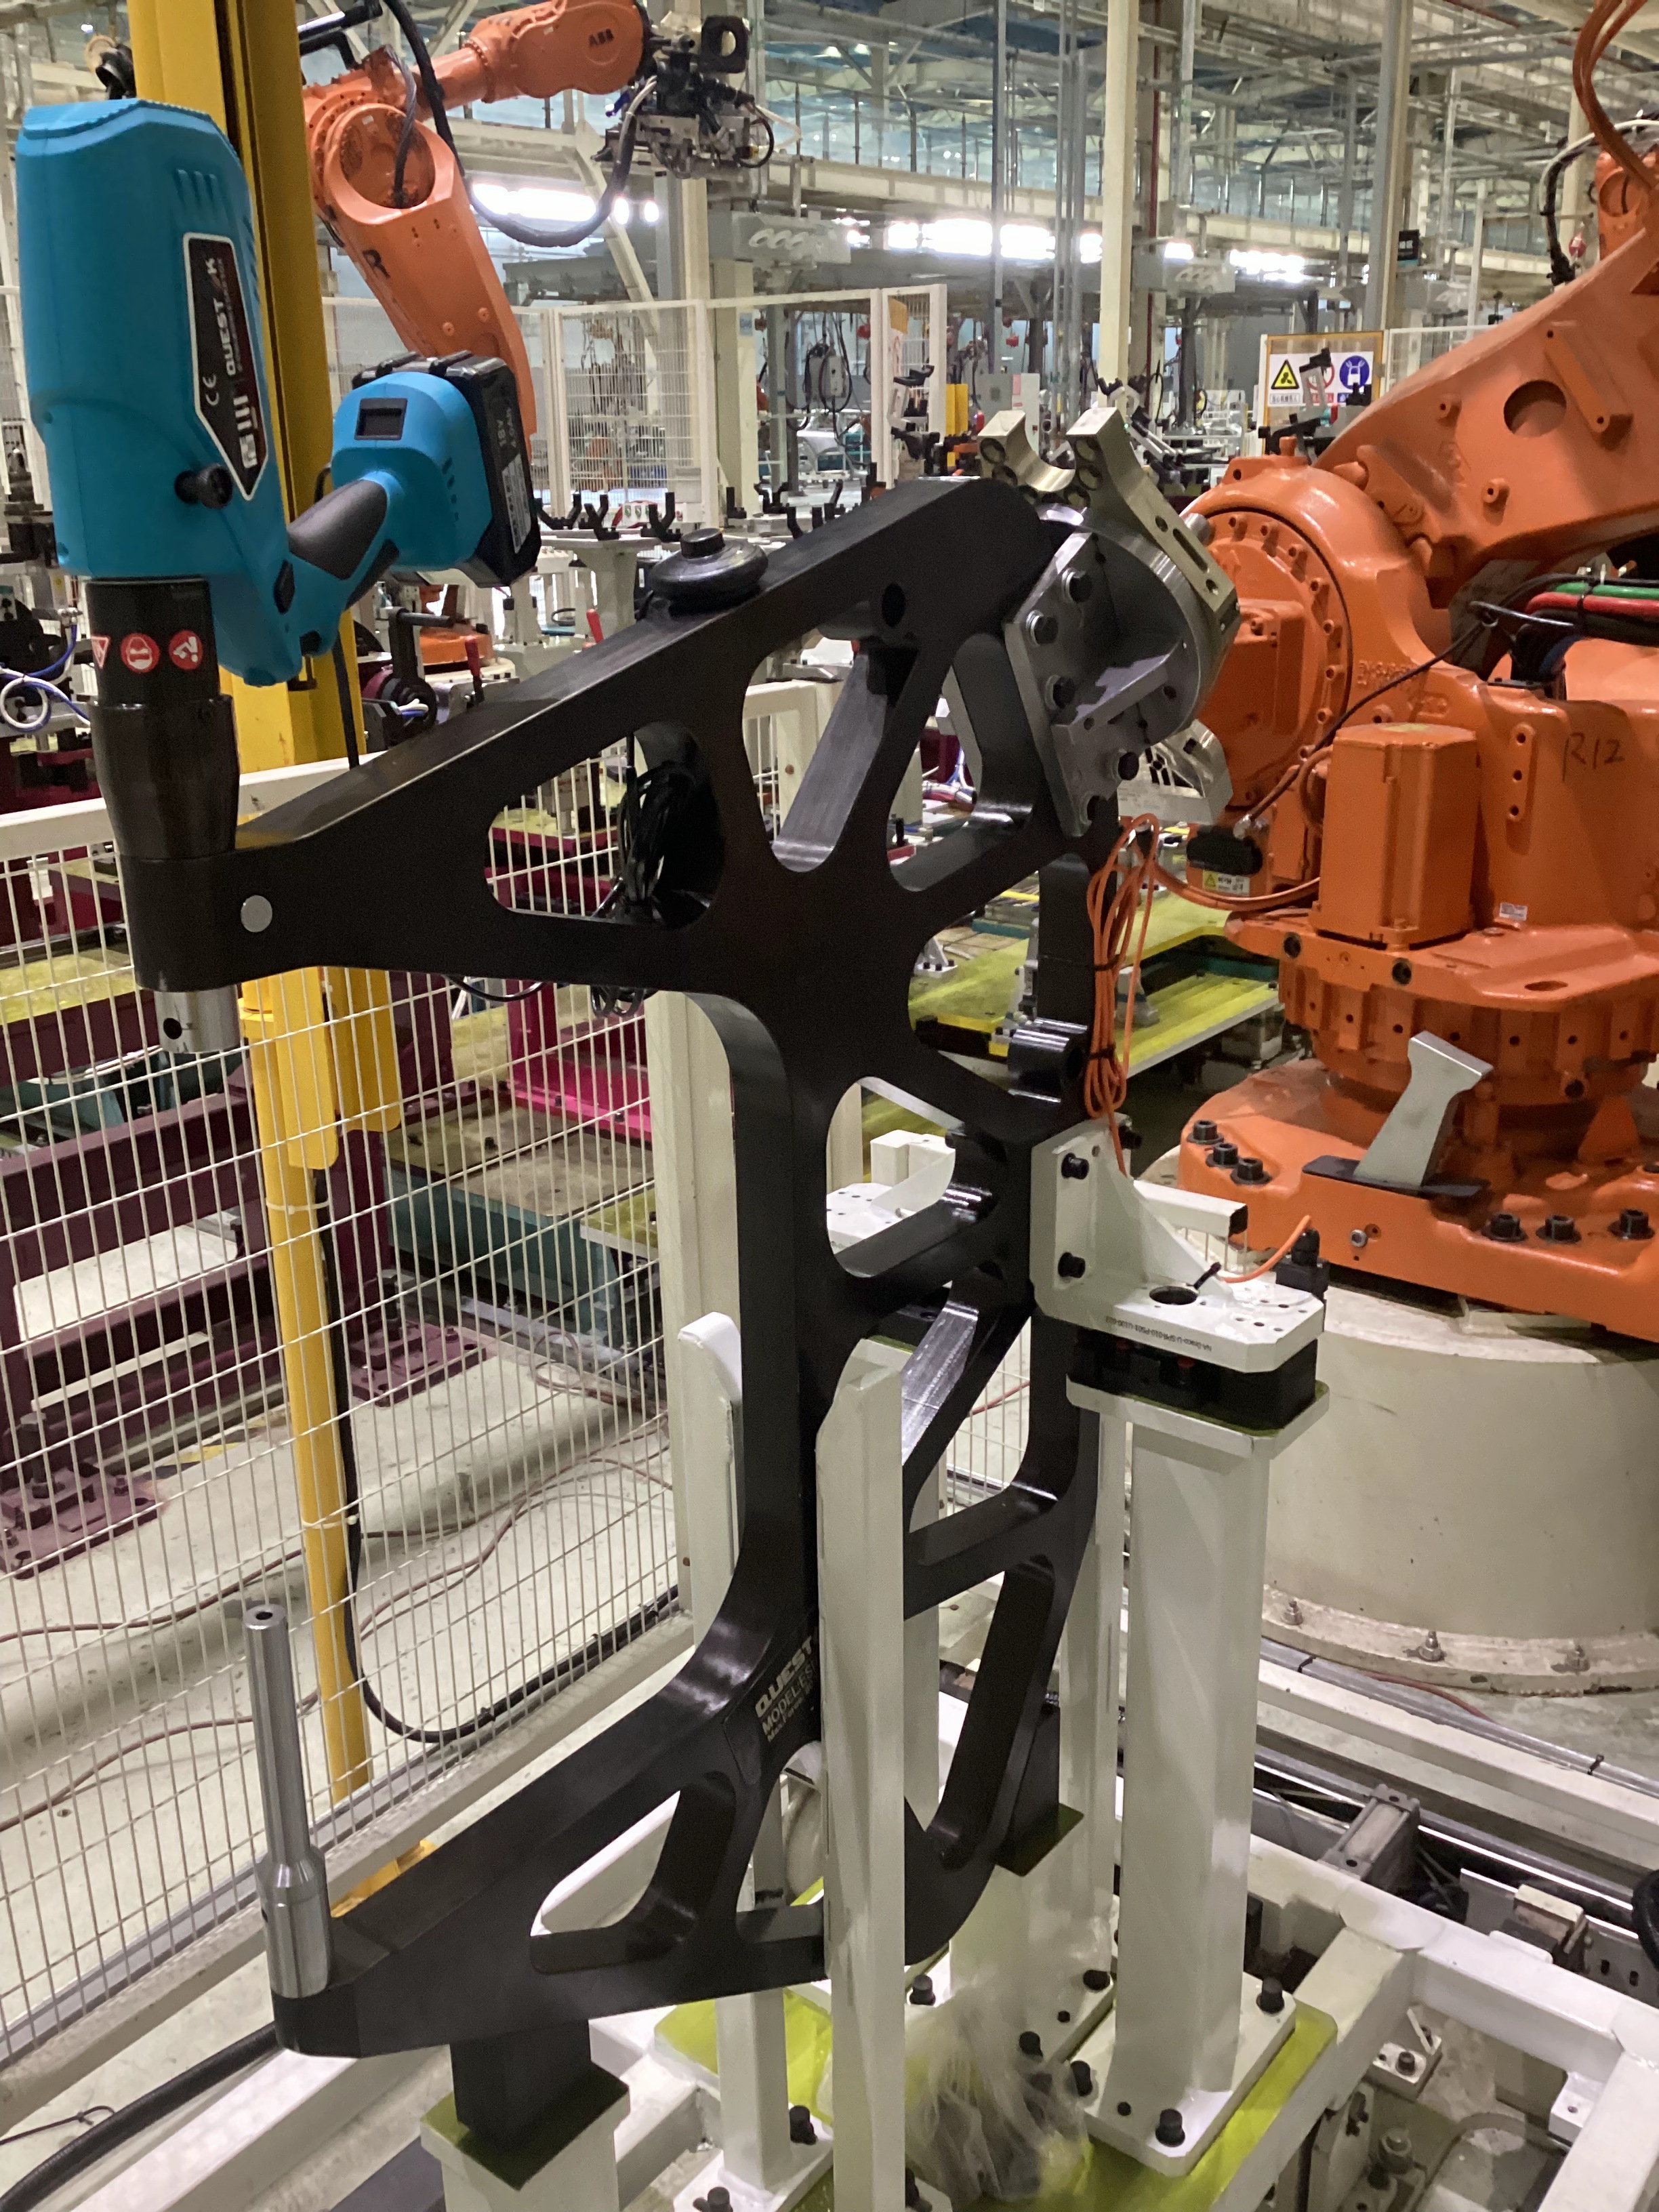
How to Verify an Auto Collision Repair SPR Gun Manufacturer: A Step-by-Step Audit Guide
Procuring reliable self-piercing riveting (SPR) equipment for modern auto collision repair requires thorough vendor vetting. Distinguishing authentic manufacturing facilities from trading intermediaries ensures high precision force execution, reliable sheet metal joining, and long-term technical support. A legitimate factory assessment involves examining engineering standards, production facilities, quality inspection processes, and official compliance documentation.
Key Verification Pillars for SPR Equipment Manufacturers
1. Regulatory Compliance and International Certifications
A authentic equipment manufacturer holds official compliance credentials registered directly under their corporate entity. Essential documentation includes valid CE certificates (such as ISETC.001120210222 and 3N210218.PTK0S25) specifically covering self-piercing riveting machinery. Additionally, Material Safety Data Sheets (MSDS) for hydraulic fluids must be provided to clear health, safety, and environmental standards across target export markets in North America, Europe, South America, and the Asia-Pacific.
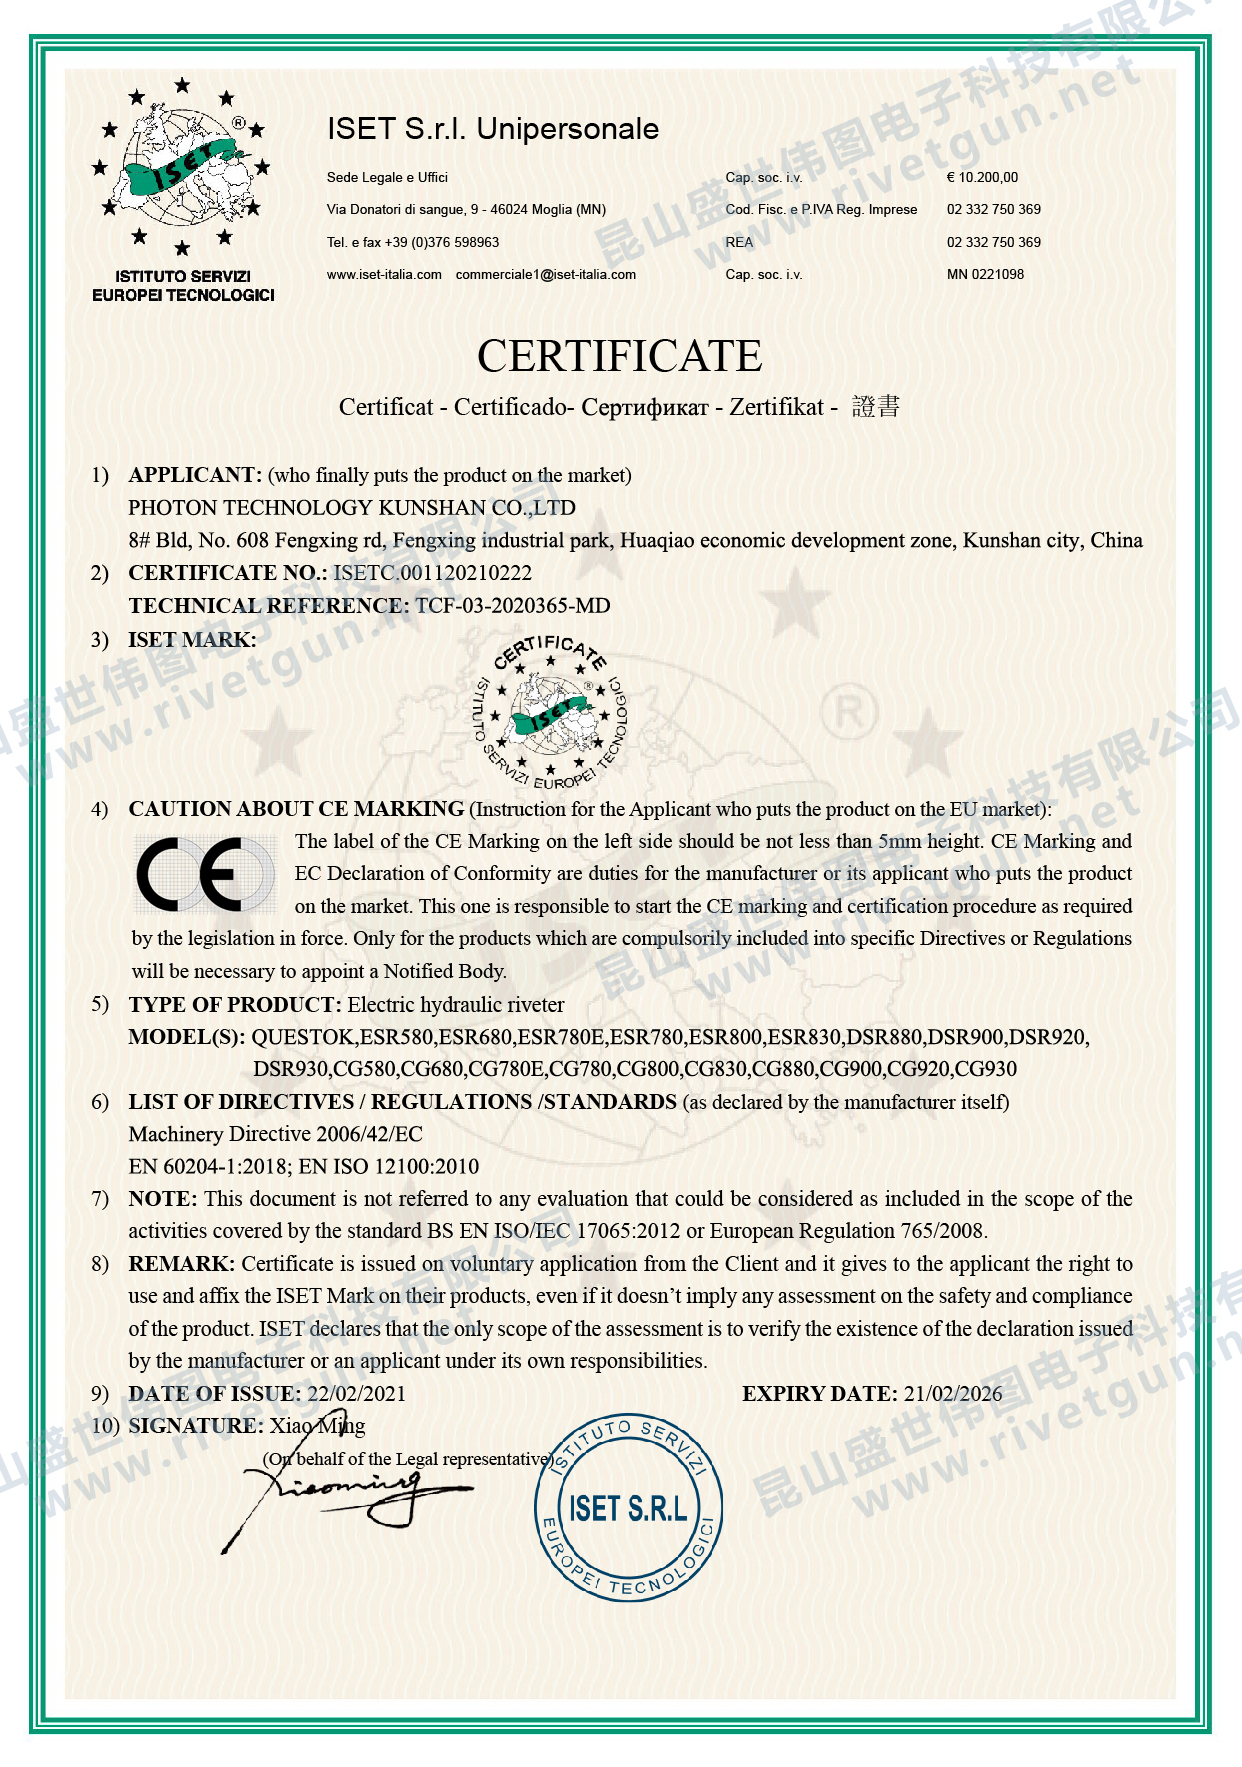
Legitimate plants regularly update these credentials and maintain technical partnerships with major original equipment manufacturers (OEMs) and tier-1 automotive suppliers, ensuring alignment with factory collision repair specifications.
2. Facility Infrastructure and Production Capacity
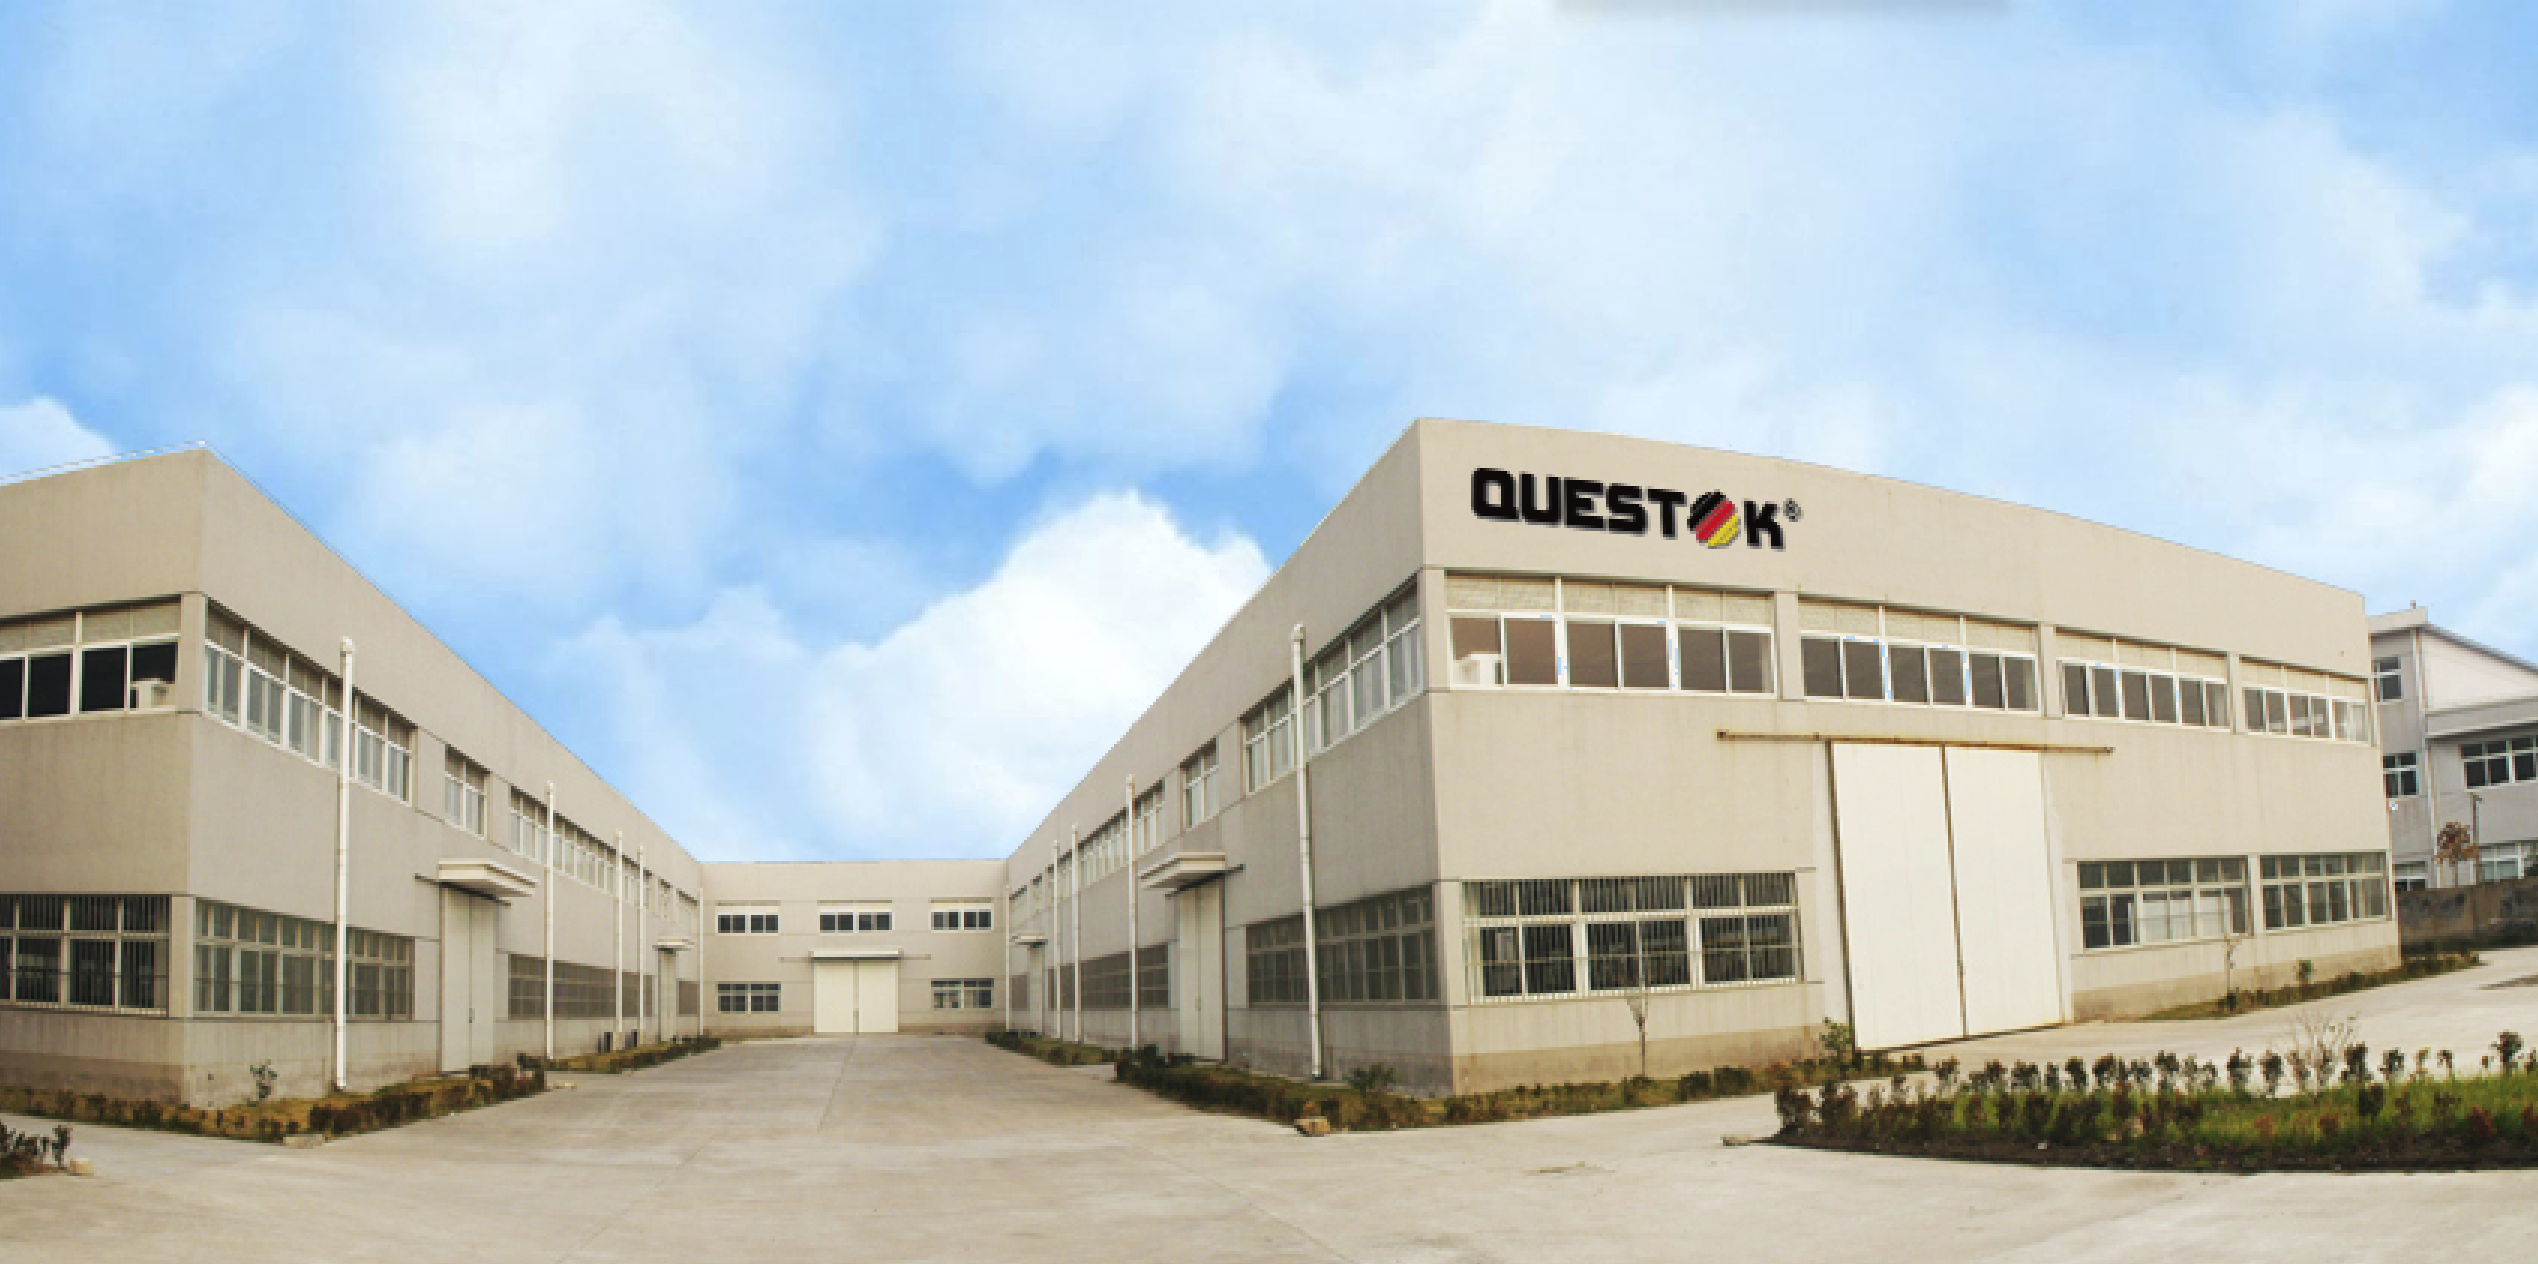
Verifying physical operational scale is critical to ensure supply chain stability. An authentic SPR gun producer operates dedicated industrial premises—such as a 5,000 square meter plant—equipped with specialized assembly lines. Reliable factories maintain a standardized output capacity exceeding 800 standard sets and 500 customized tooling configurations per month.
3. Engineering Capabilities and Vehicle Application Testing
Structural body repairs on aluminum-intensive vehicles—including models from Ford (such as the F-150), Tesla, and Mercedes-Benz—demand exact mechanical fastening without pre-drilling. Established R&D engineering teams utilize finite element analysis and hydraulic circuit design to produce tools capable of dynamic output dynamic force adjustments between 1 and 80 kN.
Proper pressure management prevents distortion on high-strength steel and aluminum alloy sheet stacks, ensuring long-term operational repeatability under body-in-white repair environments.
4. Pre-Shipment Quality Assurance and After-Sales Support
Direct manufacturers implement 100% full functional testing protocols prior to shipping. This includes delivering pressure calibration documentation along with video and photo verification of pre-dispatch testing on specified sheet metal combinations. Furthermore, genuine producers back their OEM/ODM/OBM services with a 12-hour technical response commitment and air-express dispatch for replacement components.
Factory Manufacturer vs. Trading Reseller Comparison
| Evaluation Metric | Direct Original Factory | Distributor / Reseller |
|---|---|---|
| Certifications | Direct owner of CE (ISETC.001120210222) and MSDS reports | Relies on third-party or generic supplier documents |
| Standard Delivery Time | 3 business days (orders < 100 sets) | 15 to 30 days based on external supplier stock |
| Customized Tooling Lead Time | 15 days via internal R&D engineering | 30+ days dependent on third-party factory queues |
| Quality Verification | 100% video/photo pressure calibration before dispatch | Basic packaging inspection without load testing |
| After-Sales Service | Free warranty repair & direct air-express spare parts | Delayed responses with restricted component access |
Frequently Asked Questions
Which compliance credentials confirm a legitimate auto collision repair SPR gun factory?
A genuine factory holds direct CE certifications (e.g., ISETC.001120210222 and 3N210218.PTK0S25) and valid MSDS safety documentation for hydraulic fluids, guaranteeing adherence to international safety and environmental regulations.
Why is dynamic force calibration critical for aluminum body collision repairs?
Controlling dynamic force between 1 and 80 kN prevents structural panel warping during self-piercing riveting on advanced aluminum alloys used in vehicles like the Ford F-150 or high-performance electric chassis.
What turnarounds and pre-dispatch checks indicate an authentic production facility?
Reputable facilities deliver standard models within 3 days (for under 100 units) and customized builds within 15 days, supported by complete pre-shipment video and photo functional testing.
Conclusion & Technical Support
Vetting an auto collision repair SPR gun facility requires reviewing engineering depth, production scale, and valid compliance documentation. Partnering with a manufacturer that offers 100% pre-dispatch video verification, quick lead times, flexible customization, and rapid technical support protects your workshop investment. To request customized riveting solutions or consult with technical engineers, contact us at jane@questok.com.
Company Overview
Founded in 2011, PHOTON TECHNOLOGY KUNSHAN CO.,LTD (brand Questok) operates a 5,000 sqm manufacturing plant staffed by 20 to 50 professionals. The company achieves a monthly production capacity of over 800 standard sets and 500 customized tooling systems, exporting 60% of its volume worldwide. Backed by official CE and MSDS compliance, Questok provides advanced self-piercing riveting and clinching solutions to global automotive leaders such as Mercedes-Benz, SAIC, NIO, BYD, and CATL.
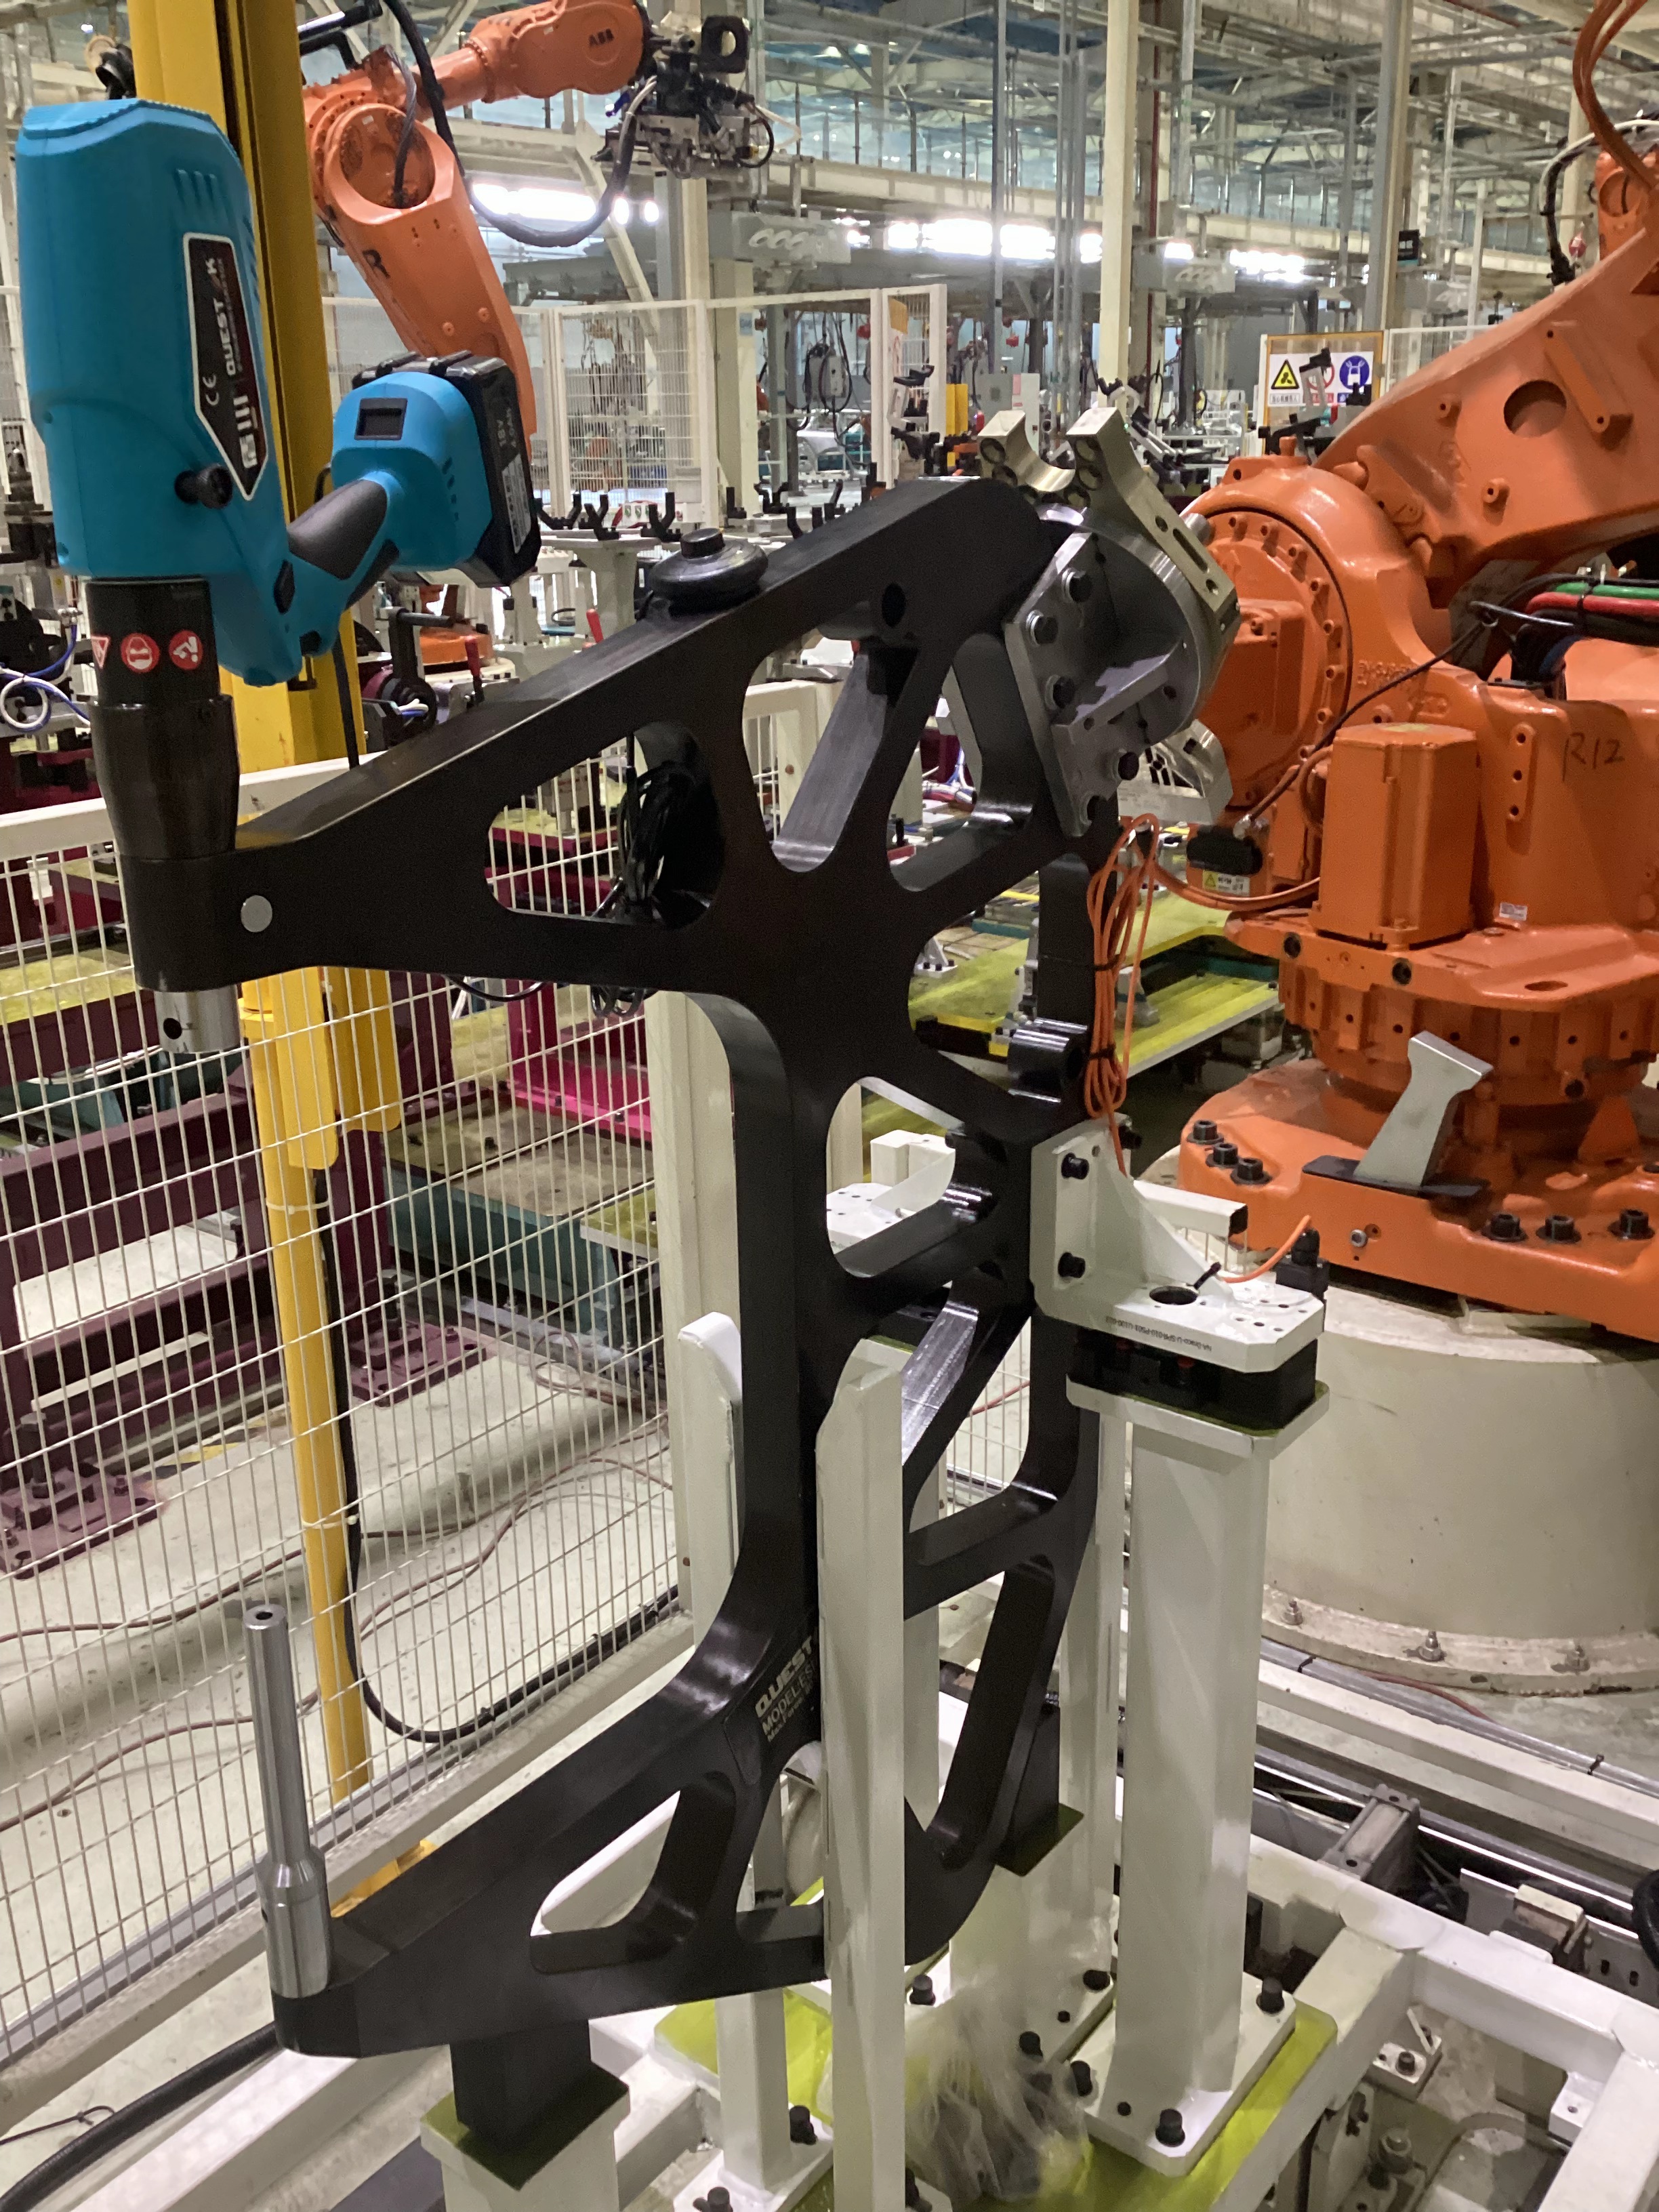
Avoiding Prototype Pitfalls: Validating Rectangular Clinching Tool Results for Mass Production
Understanding the Gap Between Prototype Testing and Mass Manufacturing
Evaluating prototype joints produced by a rectangular clinching tool often yields overly optimistic results. In controlled laboratory environments, pristine sheet metal coupons, uniform material gauges, and static pressing speeds create ideal conditions. However, when transitioning to high-volume manufacturing lines—such as commercial kitchen equipment, HVAC ductwork, commercial freezers, and control cabinet fabrication—real-world variables like coil thickness variations, surface oils, paint layers, and thermal expansion can significantly impact joint consistency and structural performance.
Essential Action Points for Validating Clinching Tools
- Evaluate joint performance using production-grade sheet metal batches and real manufacturing tolerances instead of relying solely on clean lab samples.
- Confirm single-stroke joint integrity on coated or pre-painted stainless steel panels to ensure protective layers remain uncompromised without secondary refinishing.
- Implement dynamic destructive shear and pull-out test protocols across extended production cycles to identify fluctuations caused by die wear or hydraulic pressure drift.
- Perform cross-sectional metallographic checks to verify mechanical undercut dimensions prior to integrating equipment into automated assembly environments.
In-Depth Technical Analysis: Mechanics of Joint Reliability
Achieving dependable joint quality requires understanding the complex interaction between stroke depth, press force, and die geometry. Rectangular clinching forms a cold-pressed mechanical interlock without punching through the sheet metal. To prevent misinterpreting sample success, engineering teams should analyze force-displacement curves across an adjustable 1 to 80 kN operating spectrum. An improperly calibrated press stroke can produce a button that appears sound on the outside while lacking the internal undercut depth required for structural shear strength.
Real-world application data from automated cabinet lines, including Midea control cabinet production systems, confirms that replacing conventional spot welding with single-step clinching eliminates consumable overhead while ensuring joint reliability. However, comprehensive quality control requires regular cross-sectional checks to measure neck thickness and button interlock. Utilizing equipment verified under international CE safety standards (such as certificates ISETC.001120210222 and 3N210218.PTK0S25) guarantees stable force output across continuous production shifts.
For daily operational verification, non-destructive testing provides an efficient quality control safeguard. Operators can quickly measure the button's residual bottom thickness using a specialized digital micrometer, establishing an instant indicator of proper die filling and hydraulic force delivery.
Process Comparison: Clinching vs. Alternative Joining Methods
| Evaluation Criteria | Rectangular Clinching Tool | Resistance Spot Welding | Standard Riveting System |
|---|---|---|---|
| Operational Process | Single-step cold deformation | Thermal fusion process | Multi-phase rivet insertion |
| Consumables Needed | None (rivetless process) | Welding electrodes and shield gas | External solid or blind rivets |
| Surface Refinishing | No post-process grinding or painting | Requires thermal cleanup & grinding | Flush height adjustments required |
| Layer Protection | Preserves painted and galvanized layers | Destroys surface anti-corrosion layers | Breaches protective metal coating |
| Quality Inspection | Bottom thickness & cross-section check | Destructive weld tear test | Visual setting & head inspection |
Frequently Asked Questions
Why do prototype clinching samples exhibit higher strength than production run joints?
Prototype samples are typically crafted under controlled, static conditions with ideal metal coupons. Full-scale production introduces tool heating, continuous vibration, dynamic cycle speeds, and material lot variations that can reduce joint interlock depth if pressure delivery is not strictly regulated.
What is the best non-destructive method for checking rectangular clinching joint quality?
Measuring the button's residual bottom thickness with a digital anvil micrometer gives an accurate, immediate non-destructive check of stroke calibration and metal displacement during operation.
Can rectangular clinching tools join dissimilar sheet metals without damaging surface finishes?
Yes. Rectangular clinching forms a mechanical interlock between dissimilar metals—such as aluminum and galvanized steel—without generating heat, damaging surface coatings, or requiring touch-up painting.
Summary & Recommendations
To eliminate misleading sample evaluations, engineering teams must validate rectangular clinching equipment under authentic manufacturing conditions using live production metal coils, real cycle speeds, and precise metallographic standards. Implementing pre-delivery machinery inspections and clear operating guidelines ensures consistent joint strength across HVAC, appliance, and automotive assembly lines. For tailored technical guidance or product inquiries, contact our engineering support team directly at jane@questok.com.
About Our Company
PHOTON TECHNOLOGY KUNSHAN CO.,LTD, established in 2011, operates a modern 5,000 square meter manufacturing plant driven by a skilled team of 20 to 50 specialists. The enterprise focuses on innovating advanced sheet metal joining and fastening equipment, including cordless hydraulic riveters, self-piercing riveting (SPR) systems, clinching units, and fastener insertion machines. Holding CE compliance certificates, the company delivers high-performance joining solutions to automotive, HVAC, electronics, and sheet metal fabrication industries worldwide.
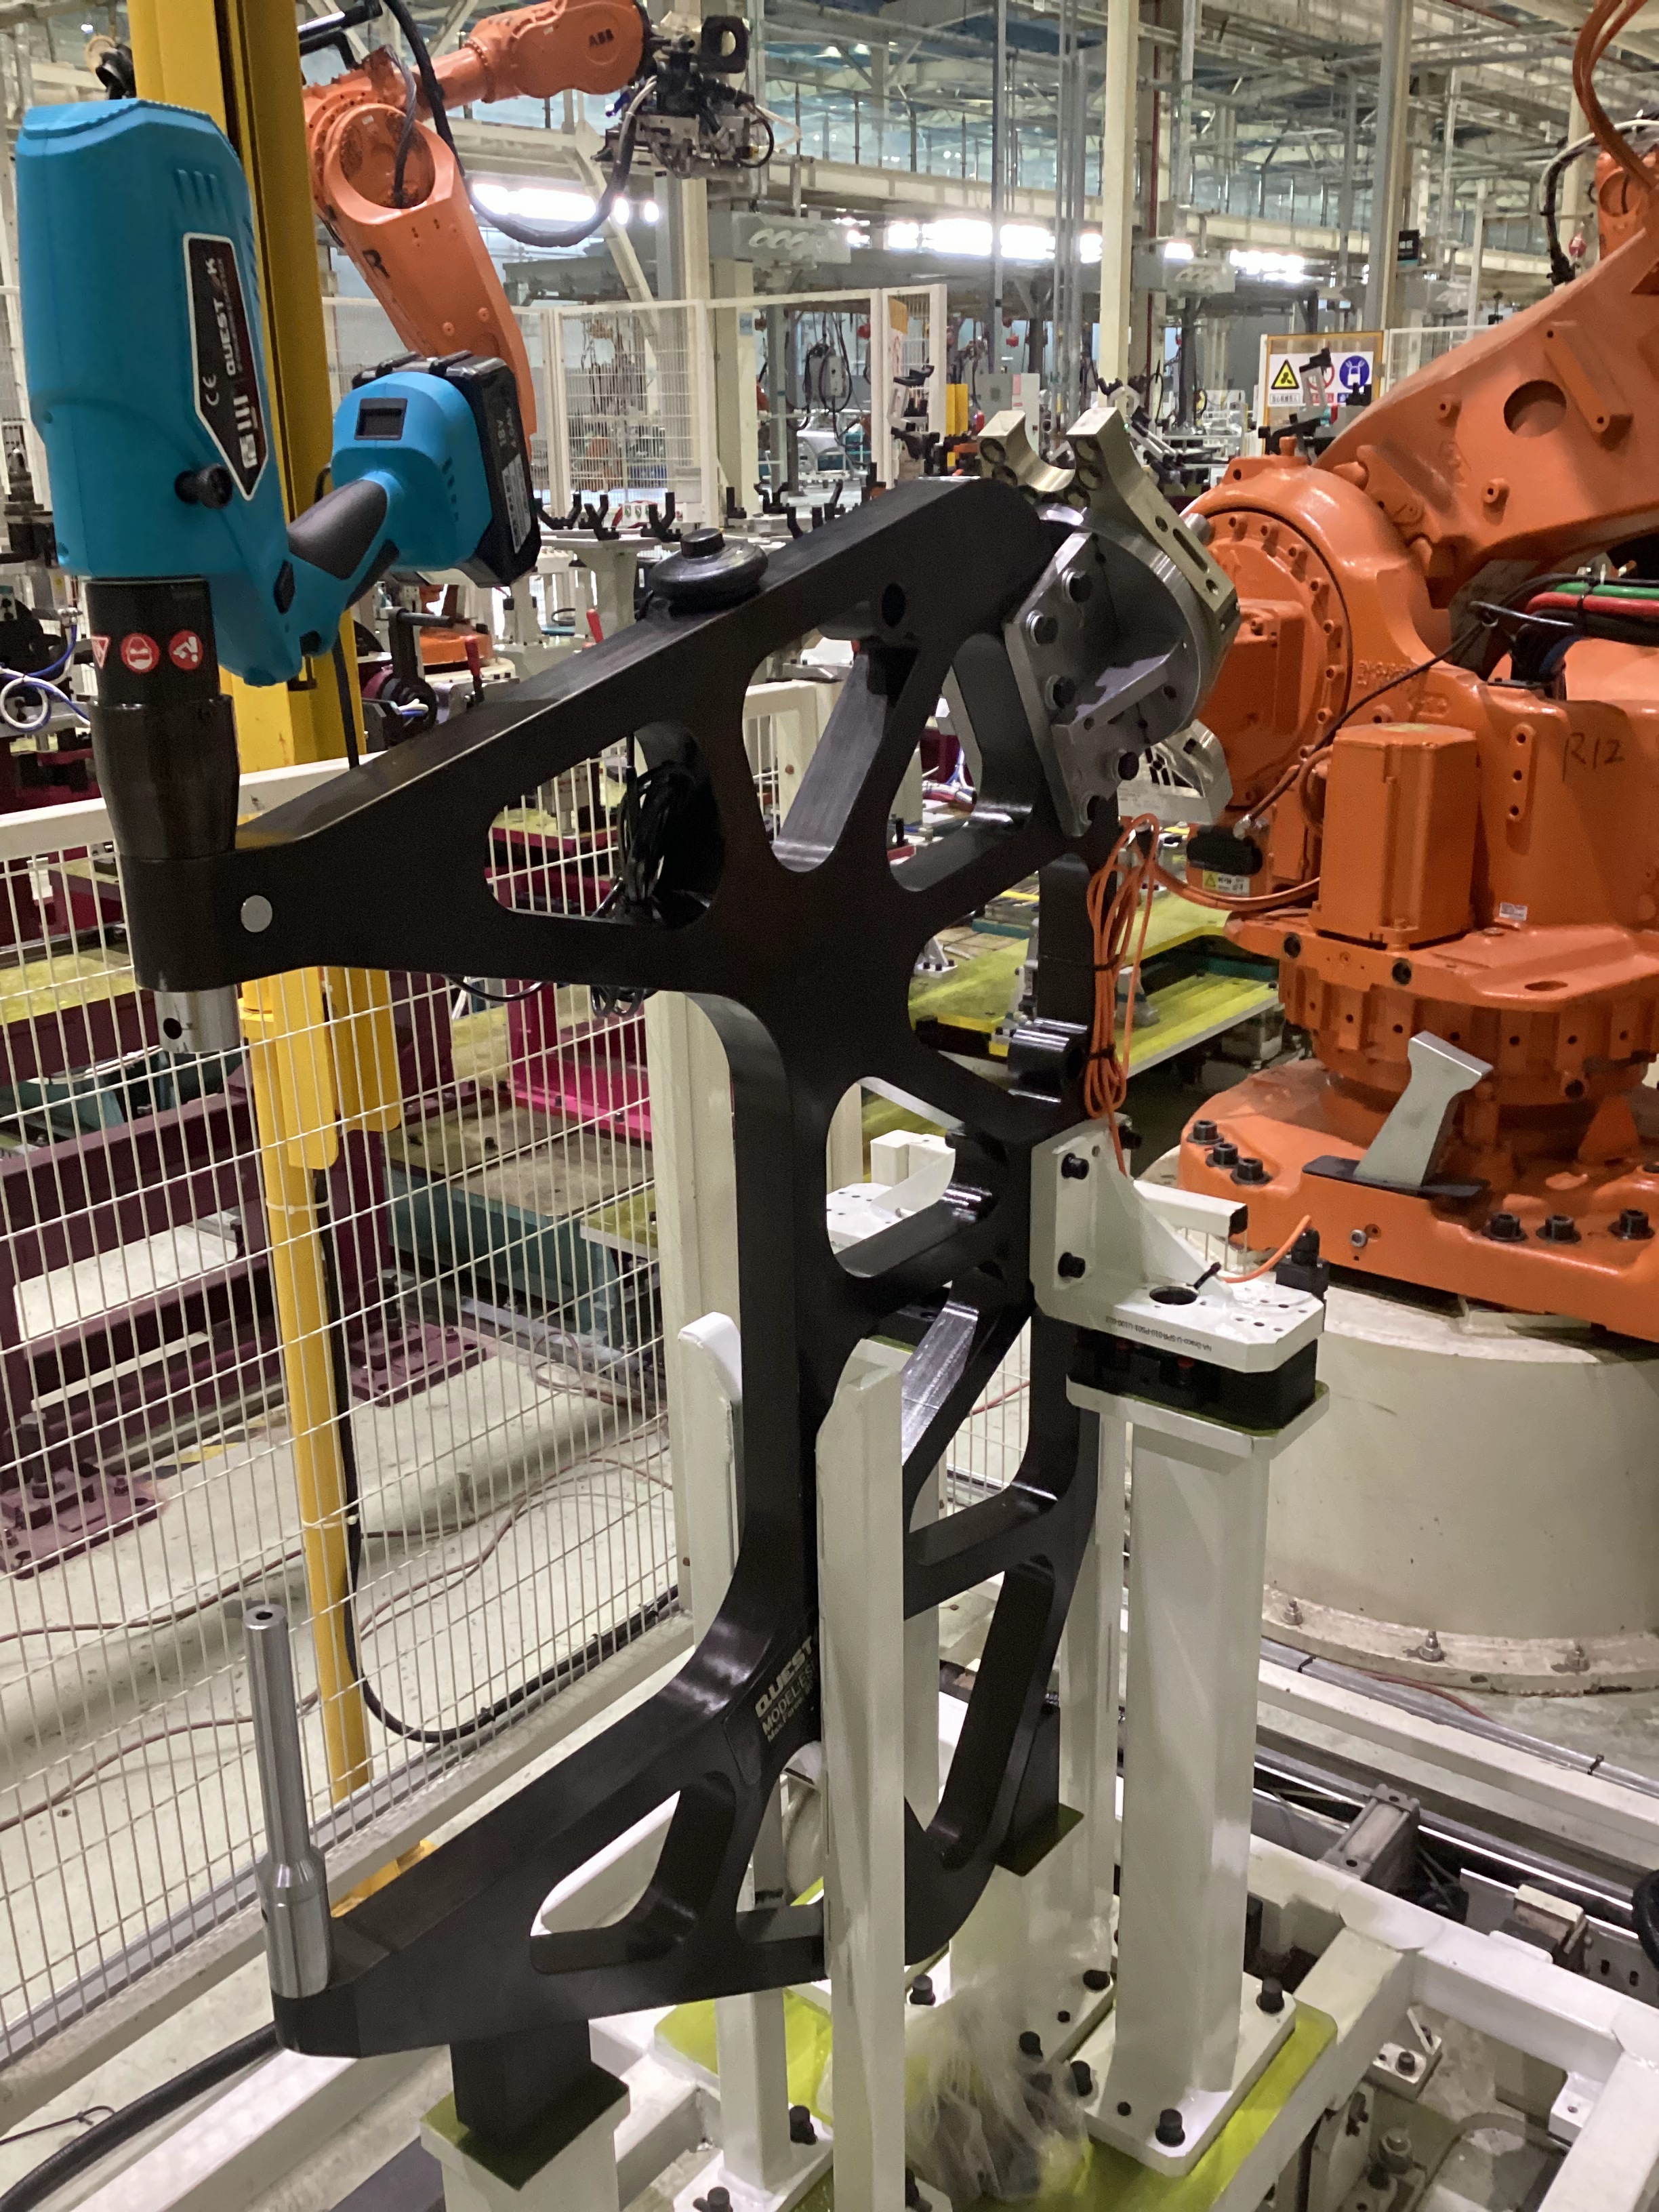
How Easily Can You Get Replacement Parts for a Handheld Clinching Gun?
Replacement parts for a handheld clinching gun can be obtained through Questok's after-sales service program. The supplier provides spare parts with equipment shipments and supports customers with fault diagnosis, video-based replacement instruction, and technical assistance. Its service information states that inquiries receive a response within 12 hours, while product materials indicate global after-sales support within 24 hours.
Replacement Support at a Glance
- Questok offers spare parts, troubleshooting assistance, and video-conference guidance for handheld clinching gun maintenance.
- When additional parts are needed after the supplied spares have been used, the company states that replacements can be shipped by air with installation support.
- These clinching tools are intended for automotive sheet metal brackets, covers, HVAC ducts, control cabinets, white goods, commercial kitchens, and commercial freezers.
- For HVAC production, the equipment can be used with ductwork, air fans, dampers, filters, and flanges.
How the After-Sales Process Works
Access to replacement components depends on both the machine design and the supplier's service process. Questok says that spare parts are supplied with delivered equipment, helping customers address common maintenance requirements. If a fault occurs, its support team can provide troubleshooting guidance and explain replacement procedures through a video conference.
If the original spare parts have already been used, Questok states that further components may be dispatched by air. Technical personnel can assist with installation after the shipment arrives. When a customer cannot complete the repair locally, the machine may be returned to Questok for service and then sent back by air express. The company describes the repair service as free; for warranty cases, related expenses are fully covered, while out-of-warranty customers are responsible for freight and replacement-part charges.
Equipment Specifications and Delivery
The handheld model is an electric clinching gun with an output pressure range of 1-80 kN and adjustable forming pressure. For orders below 50 sets, the stated standard delivery time is 3 days after payment. Customized orders are listed with a 15-day lead time. The minimum order quantity is 1 set, and the quality process includes full inspection.
Questok reports application experience in vehicle repair and HVAC joining. Its clinching technology enables one-step joining without consumables for the listed HVAC applications, and the finished joint does not require polishing or repainting. Reported cooperation examples include control cabinet manufacturing for Midea, as well as joining solutions for automotive and electric vehicle battery manufacturers.
The company also lists CE certificates ISETC.001120210222 and 3N210218.PTK0S25 for its clinching guns, clinching tools, and related fastening equipment. MSDS documents are listed for the same product categories.
Service and Supply Comparison
| Service or equipment factor | Available information |
|---|---|
| Replacement parts | Available through the supplier; additional spares can be shipped by air when necessary. |
| Replacement guidance | Available through troubleshooting support and video-conference instruction. |
| Complex repair | The machine can be returned for repair when the customer cannot complete the work locally. |
| After-sales response | Business information cites replies within 12 hours, while product information cites global support within 24 hours. |
| Standard product delivery | 3 days after payment for quantities below 50 sets. |
| Customized product delivery | 15 days for customized orders. |
Frequently Asked Questions
Are replacement parts available for a handheld clinching gun?
Yes. Questok says it supplies spare parts and can arrange air shipment of additional components when the original supplied parts are no longer sufficient.
Can customers receive help with part replacement?
Yes. The service process includes fault-finding assistance and video-conference guidance for replacing spare parts.
What if a local repair is not possible?
In exceptional situations, Questok states that the machine can be sent back for repair and returned by air express. Repair service is described as free, while freight and spare-part expenses depend on the warranty status.
Conclusion
Based on Questok's published after-sales process, replacement parts for its handheld clinching guns are obtainable, with options for spare-part supply, air delivery, troubleshooting, and video instruction. The company supports ODM and OBM projects, accepts orders starting at 1 set, and states that products receive full inspection. For technical assistance or application-specific solutions, contact jane@questok.com.
About Us
PHOTON TECHNOLOGY KUNSHAN CO.,LTD, operating under the Questok brand, develops fastening, joining, and assembly equipment for industrial manufacturing. Founded in 2011, the company produces SPR riveting systems, self-piercing riveting guns, clinching guns, clinching equipment, fastener pressing tools, and associated assembly solutions. Its stated production capacity is 800 standard models and 500 customized models, serving customers in several manufacturing sectors.
Its listed credentials include CE certificates ISETC.001120210222 and 3N210218.PTK0S25.
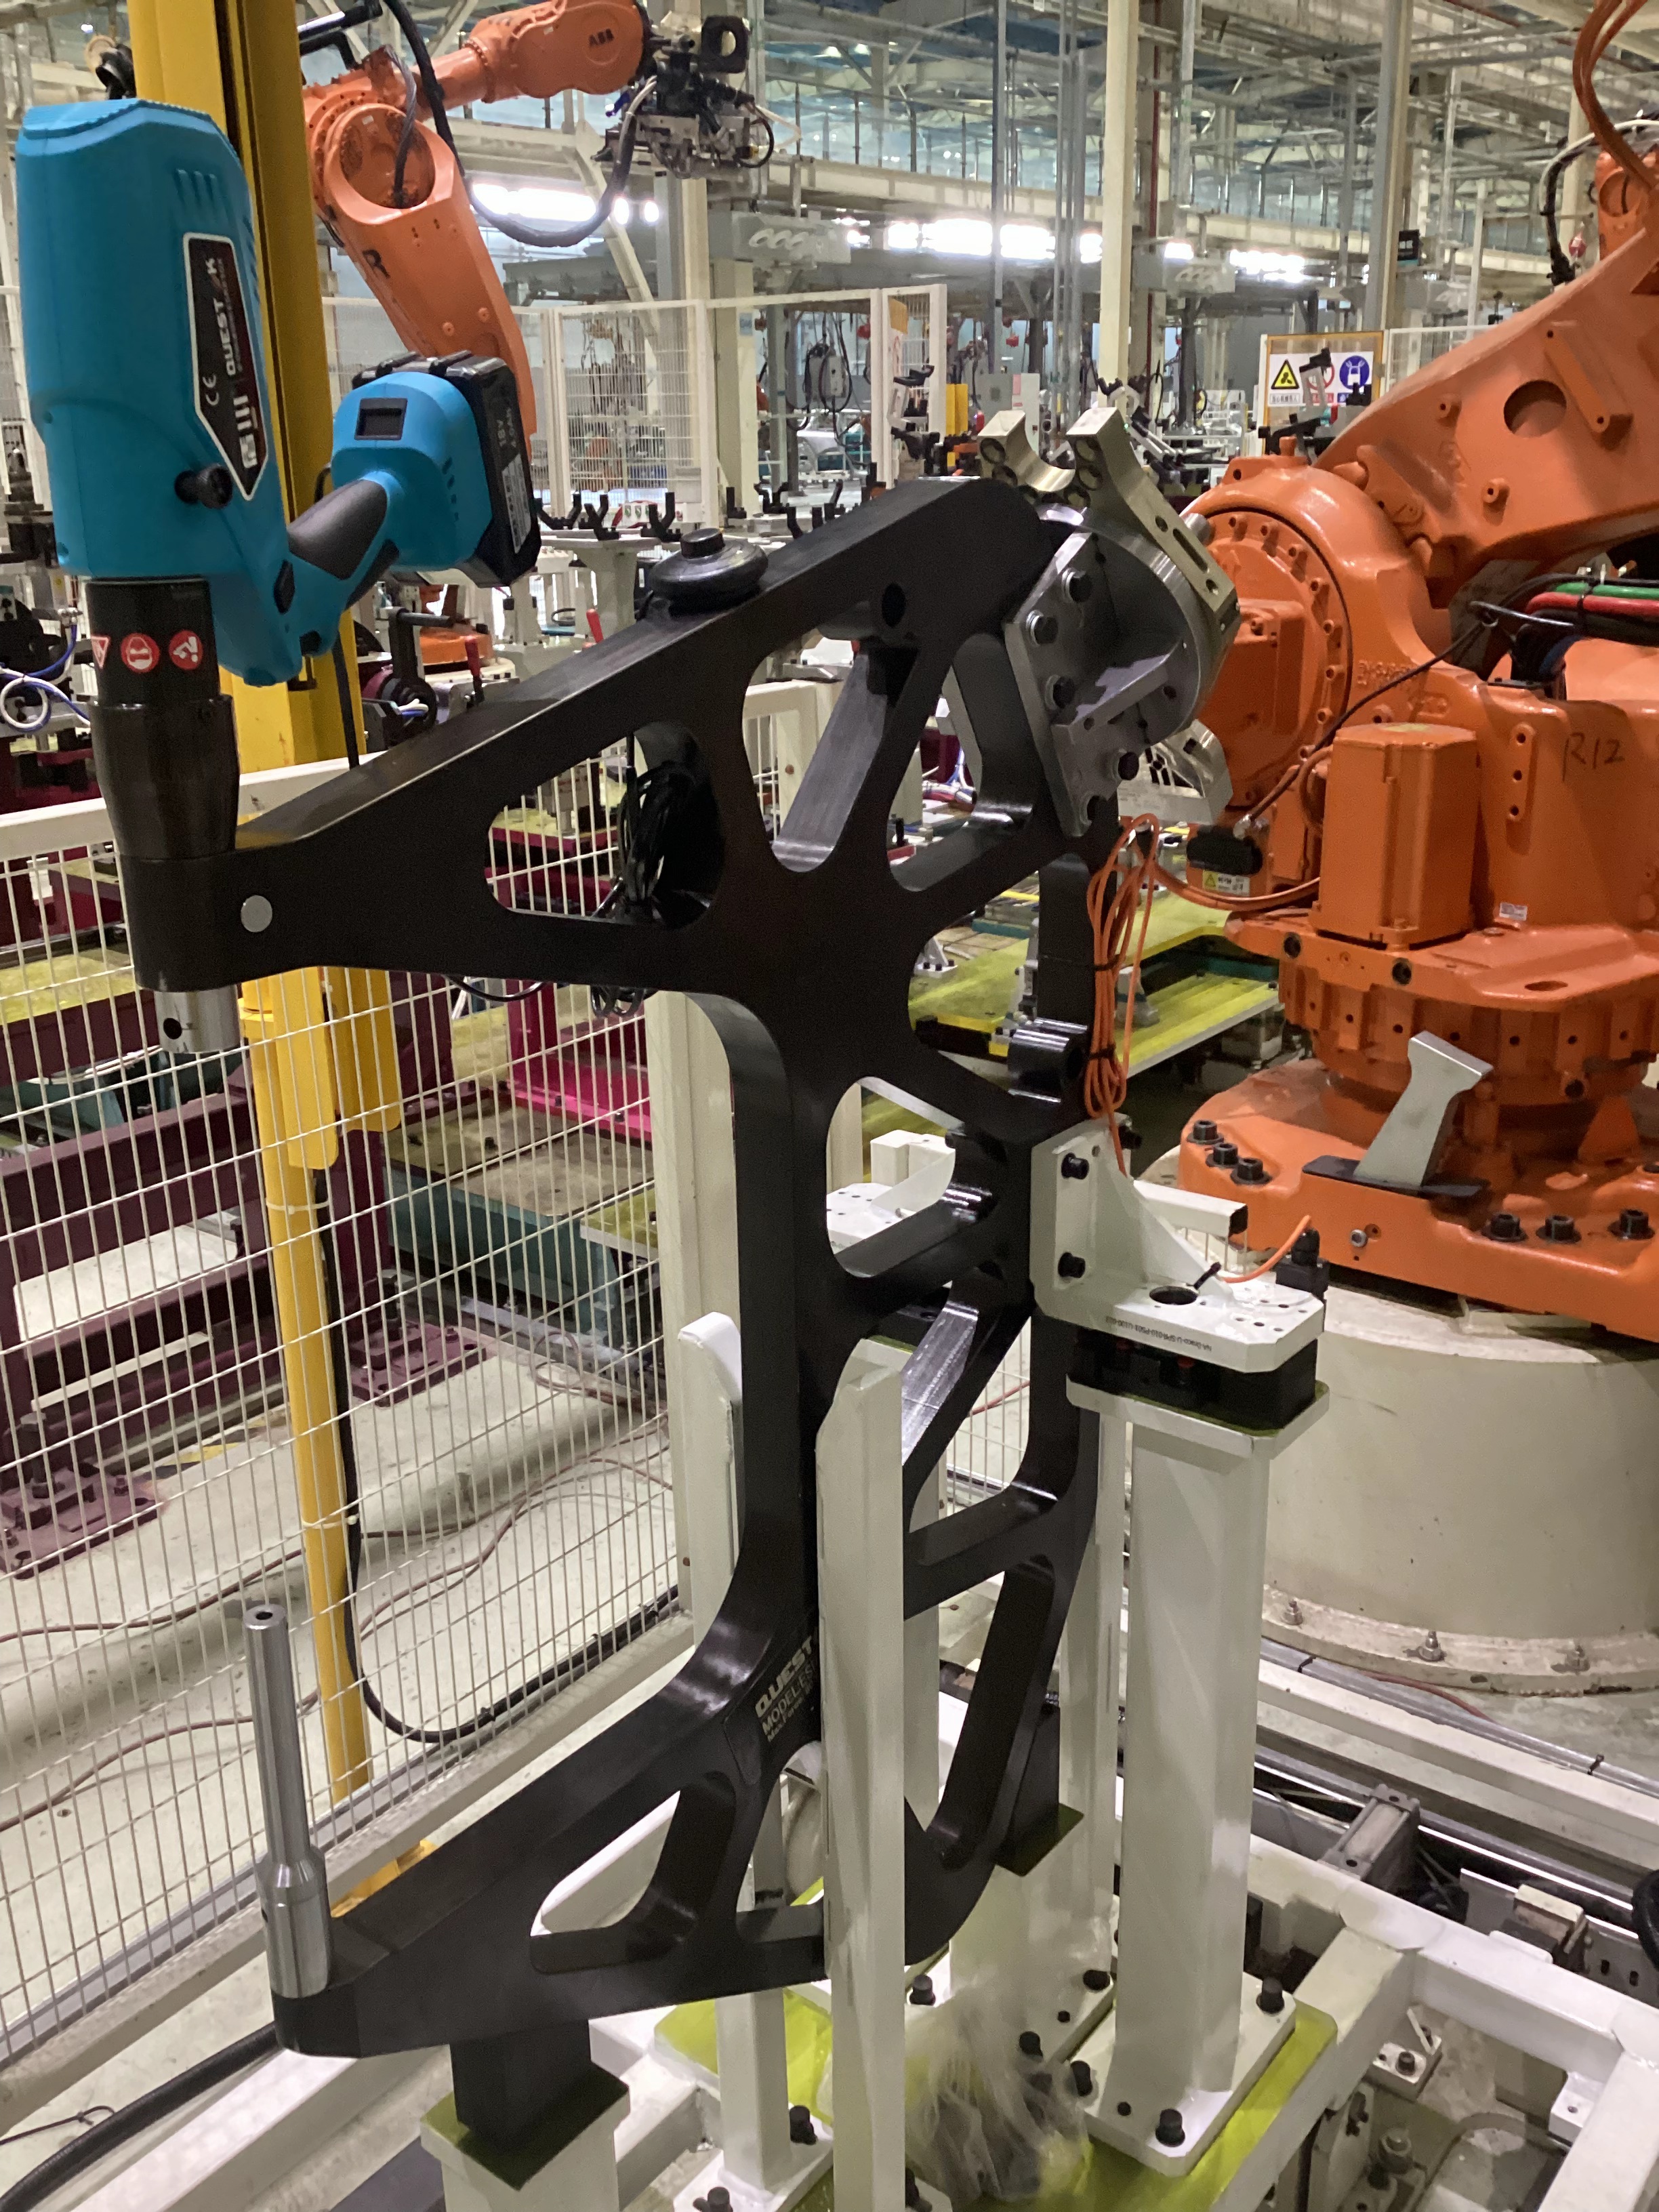
Should You Arrange a Third-Party Audit When Sourcing an SPR Riveting Gun?
A third-party audit can provide independent assurance when evaluating an SPR riveting gun supplier. It is best used alongside direct checks of the equipment, documentation, and supplier’s ability to meet your production needs. Key areas to review include certifications, quality controls, manufacturing capacity, delivery schedules, technical assistance, and experience with similar joining applications.
When an Independent Audit Adds Value
Consider an audit when you need external confirmation of factory capability, quality procedures, or supplier records. An audit does not replace application testing or a review of the supplier’s own documentation; it helps verify that the stated processes and resources are in place.
For Questok, buyers can assess the supplier’s listed CE credentials, inspection procedures, SPR application history, and after-sales commitments as part of this review. The company identifies itself as PHOTON TECHNOLOGY KUNSHAN CO.,LTD and supplies fastening and joining equipment, including SPR riveting guns and systems, self-piercing riveting tools, clinching equipment, fastener pressing tools, and integrated solutions.
Technical and Application Checks
The product specification gives an output pressure range of 1-80 kN, with precise pressure adjustment. It is described for bus, RV, and special-vehicle assembly. Questok also reports experience with automotive production, including aluminum vehicle bodies, EV battery trays, and water cooling plates. Buyers should confirm that the proposed configuration and joining process suit their materials, part geometry, and production requirements.
Documents, Quality, and Support
The supplier’s listed credentials include CE certificates ISETC.001120210222 and 3N210218.PTK0S25, as well as MSDS certificate 262620110732. The stated applicability covers SPR, self-piercing riveting, clinching, and fastener pressing product categories. During sourcing, verify each certificate’s authenticity, scope, and relevance to the specific equipment being purchased.
Questok describes its quality process as full inspection from incoming materials through finished products, with functional tests before shipment. The company also says it can share test videos and photos with customers. Its stated after-sales provisions include replies within 12 hours at the company level, spare-parts assistance, video-call troubleshooting, and free repair service. The product information separately states a global after-sales response within 24 hours; confirm which service commitment applies to your order.
Reported project experience includes prototype and pilot production for EV and automotive manufacturers, an automotive line using both self-piercing riveting and rivetless clinching, and an automated control-cabinet line using clinching. These examples suggest experience with tailored joining projects, but they do not remove the need for application-specific trials and acceptance criteria.
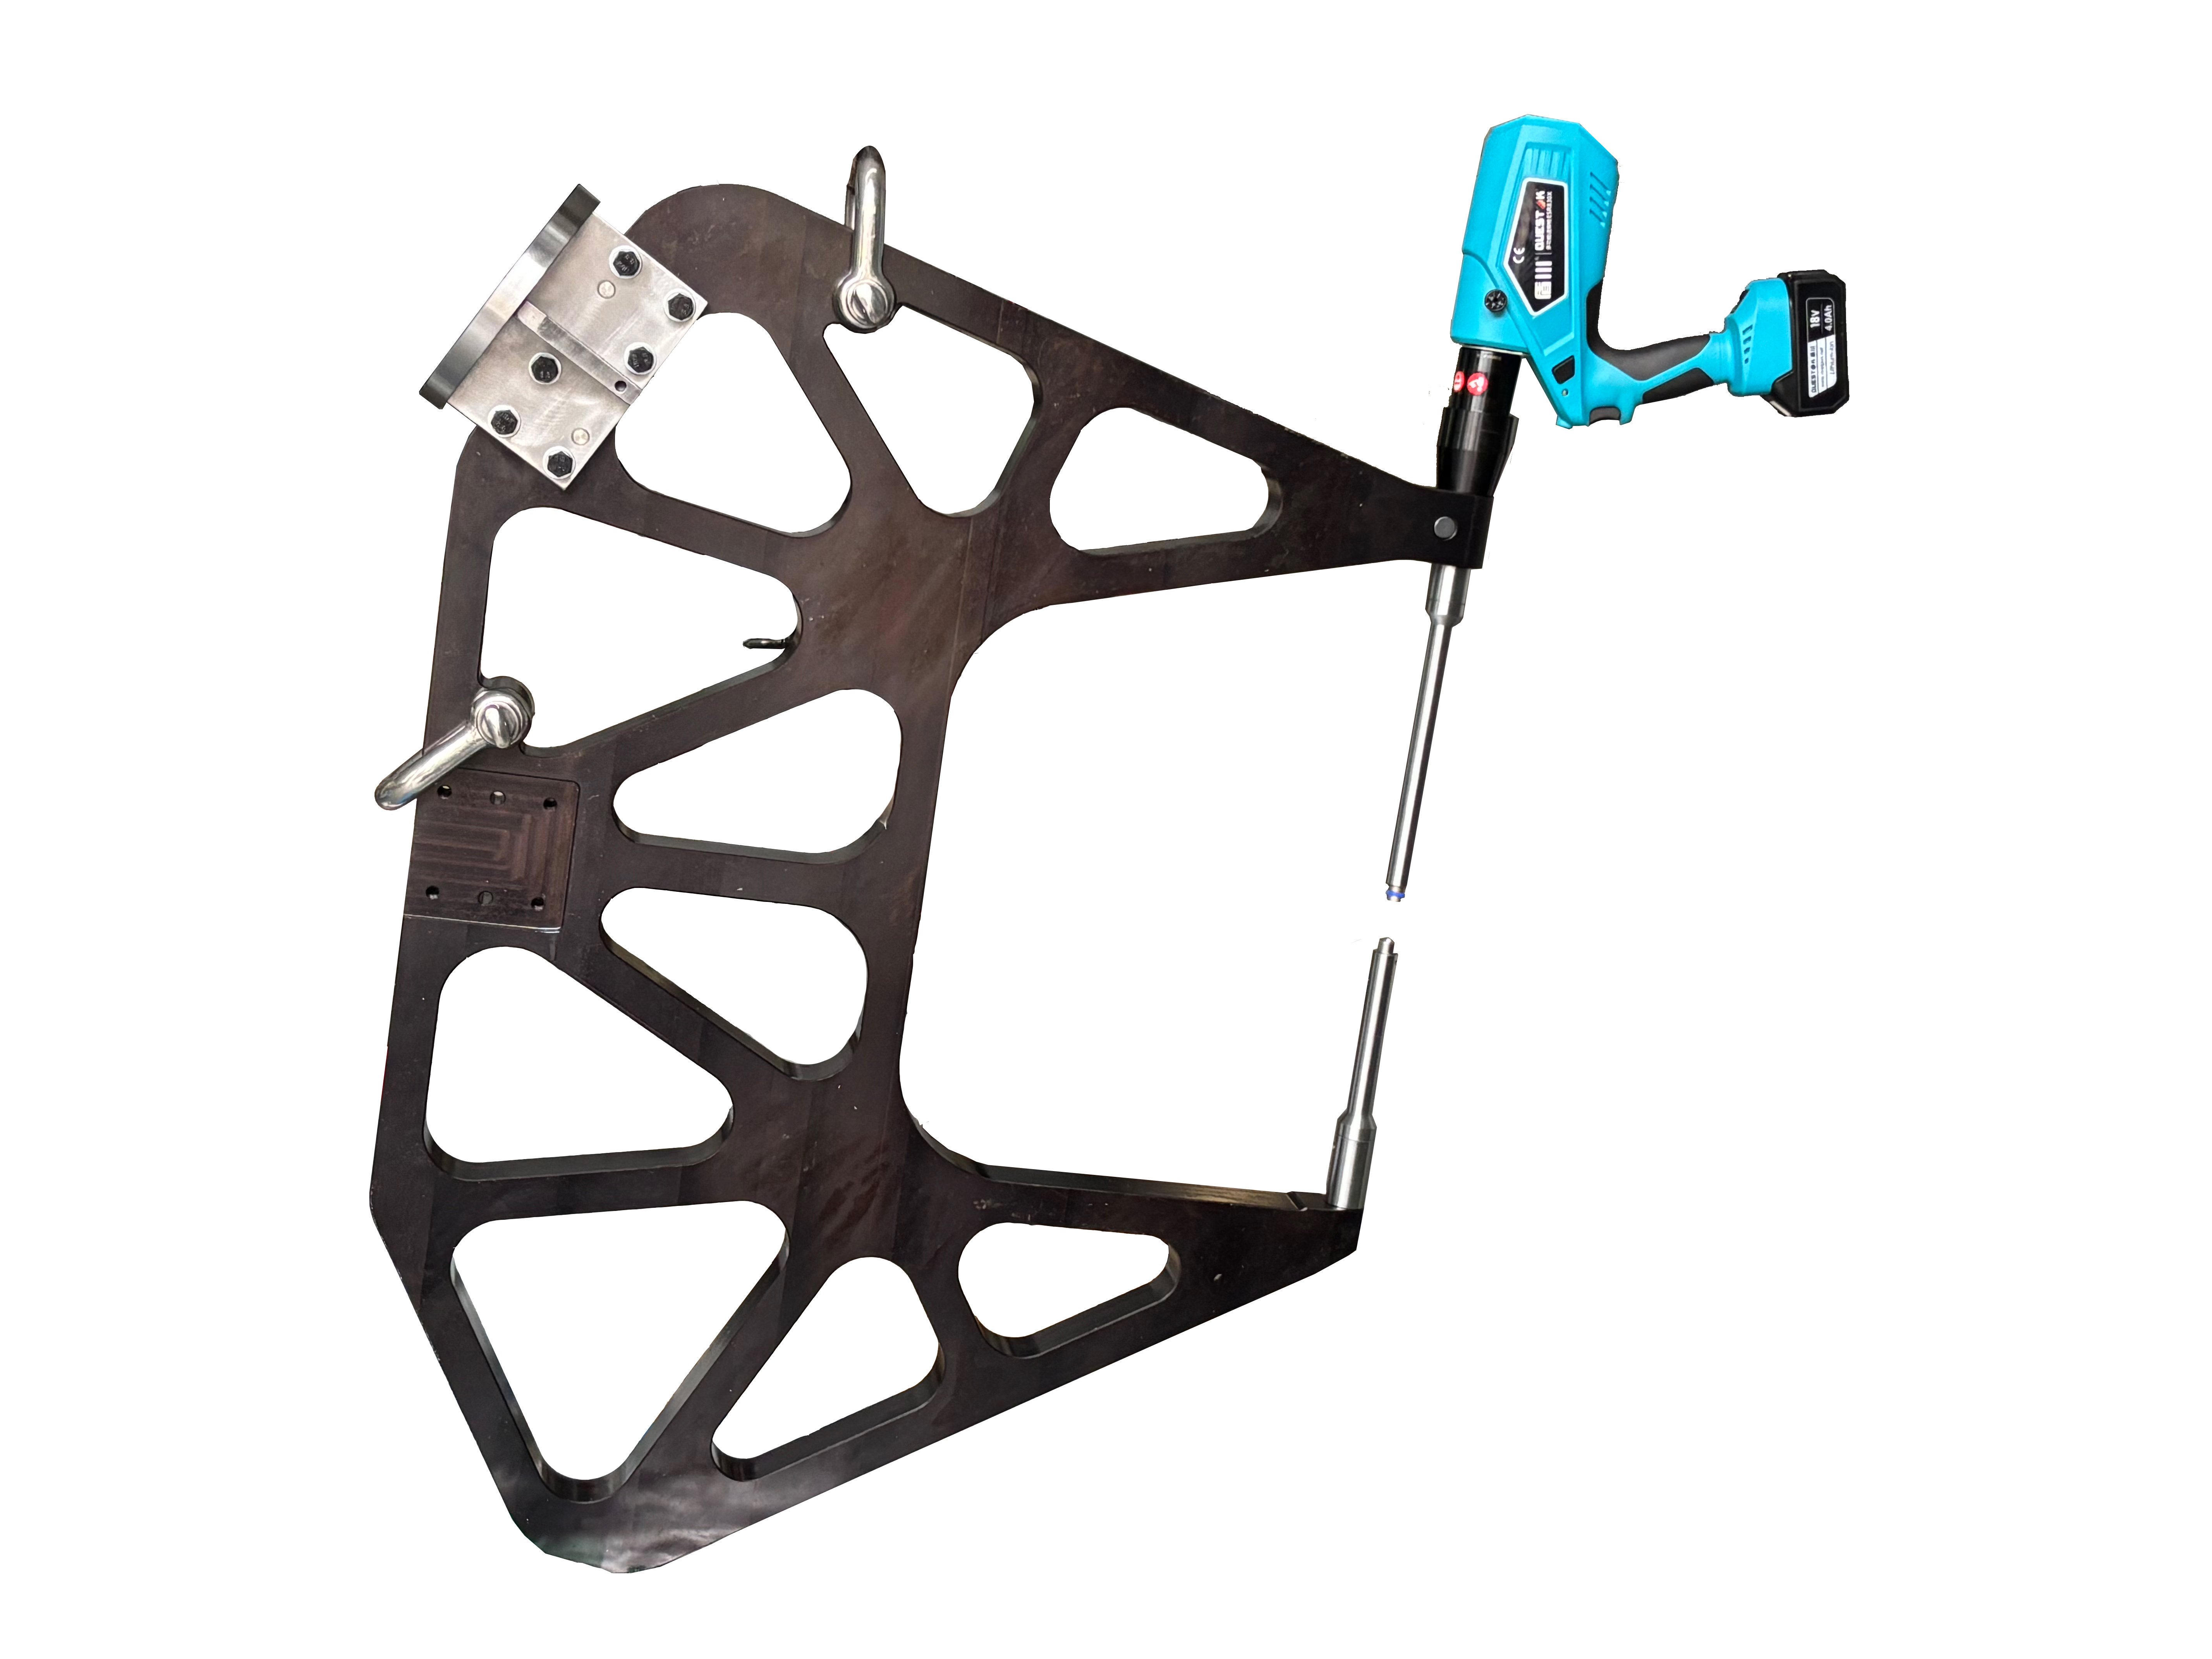
Audit Scope and Sourcing Details
| Area to verify | Information provided | What an audit can confirm |
|---|---|---|
| Equipment capability | 1-80 kN output pressure with precise adjustment | Whether the supplied configuration and supporting records match the specification |
| Quality controls | Full inspection, functional testing, and customer-shared test media | Whether inspection steps are documented and followed in production |
| Certifications | CE certificates and an MSDS certificate are listed | Certificate validity, scope, and relevance to the ordered product |
| Capacity and delivery | Monthly capacity stated as 800 standard sets and 500 customized sets | Available resources and whether the quoted schedule is achievable |
| Service support | Spare parts and troubleshooting support; response times of 12 or 24 hours are stated | Service staffing, parts availability, and records supporting the applicable commitment |
The stated minimum order quantity is one set. For orders below 50 sets, standard models are listed for delivery within three days after payment; customized solutions are listed at 15 days. Confirm that these lead times apply to the required configuration and shipment terms. Questok reports support for ODM and OBM arrangements and accepts T/T, PayPal, credit card, and Alipay. Shipping options include air express, air cargo, and ocean freight.
Frequently Asked Questions
Is an audit mandatory before purchasing an SPR riveting gun?
The available supplier information does not specify that an audit is required. It can be a useful additional measure when you need independent evidence about factory operations, quality, certifications, capacity, or service.
Which points should the audit cover?
Review the adjustable 1-80 kN output, product configuration, inspection and functional-test records, applicable CE documentation, production resources, delivery planning, spare-parts process, and experience with automotive or EV joining applications.
Can I purchase one unit for evaluation?
Yes. The stated MOQ is one set. Standard models are listed for delivery within three days after payment for orders below 50 sets, while customized solutions are listed at 15 days. Verify the schedule for your specific order before confirming.
Recommendation
Use a third-party audit when independent supplier evidence matters, particularly for customized automotive or EV production. Pair it with product and application trials, certificate checks, review of inspection records, and confirmation of delivery and support arrangements. For technical details or assistance, contact jane@questok.com.
About Questok
PHOTON TECHNOLOGY KUNSHAN CO.,LTD, operating as Questok, develops fastening, joining, and assembly equipment for manufacturing. Its stated product range includes battery-powered hydraulic riveting tools, SPR systems, self-piercing riveting guns, clinching equipment, and fastener pressing and assembly solutions. Established in 2011, the company reports a 5,000 sqm factory and monthly capacity of 800 standard models and 500 customized models. Its listed credentials include CE and MSDS certificates, with reported projects in automotive, EV battery, and automated manufacturing.
REPORT