




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Factory Audit Checklist for a Fasteners Press Tool Manufacturer
Auditing a manufacturer of press tools for fasteners requires more than checking equipment appearance or quoted prices. The review should cover engineering capability, hydraulic performance, production controls, material traceability, inspection records, customization, certifications, delivery reliability, and technical service. For a rivetless clinching gun, particular attention should be paid to the claimed 30–60 kN output range, accurate force adjustment, complete testing, fast delivery, and support availability within 24 hours.
What to Evaluate During the Factory Audit
- Ask how the supplier manages mechanical design, hydraulic circuits, motor drive, electrical control, tooling, assembly, calibration, and final functional testing.
- Confirm the factory’s ability to manufacture both standard and engineered solutions. The stated production capability exceeds 800 standard sets and 500 customized sets, subject to order requirements.
- Review experience in HVAC sheet-metal joining, automotive manufacturing, EV battery trays, water cooling plates, and other applications that resemble your materials and joint designs.
- Verify the inspection system, certification coverage, ODM and OBM services, minimum order quantity, delivery commitments, and after-sales escalation process.
Product Performance and Joining Process Verification
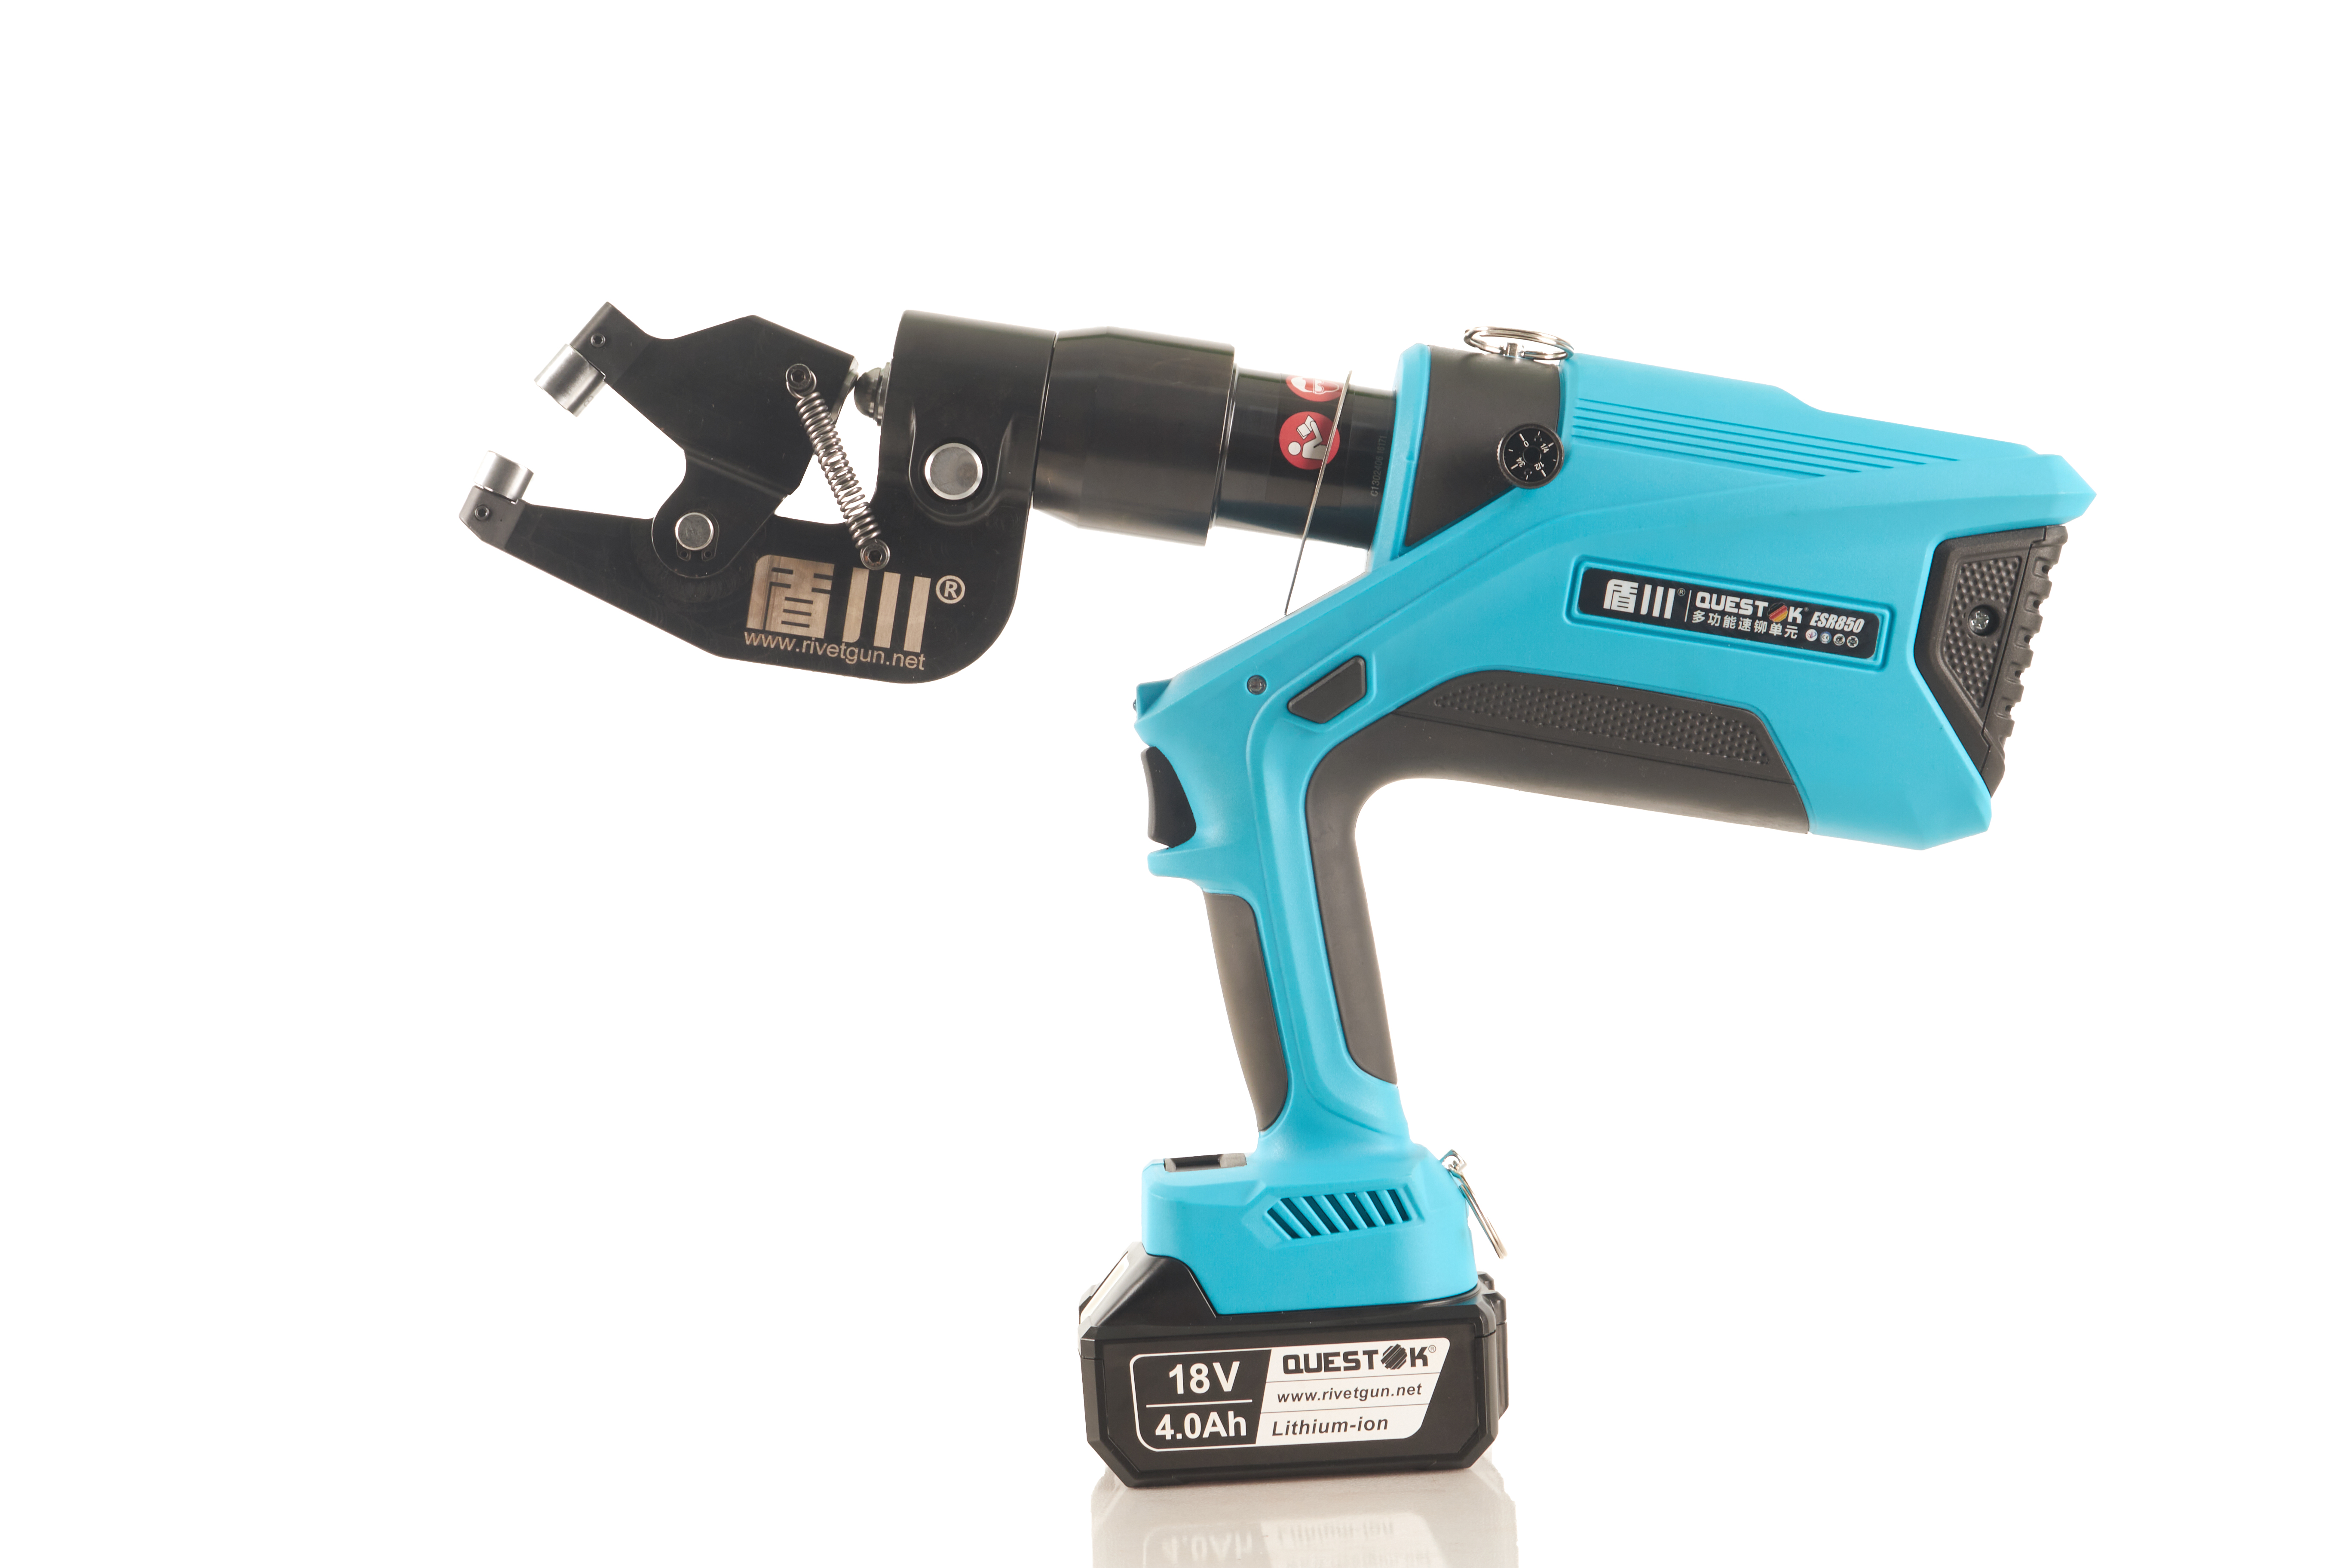
Begin with a technical demonstration of the QUESTOK Rivetless Clinching Gun for Modular Housing Plumbing Bracket Joining. Ask the manufacturer to show how the hydraulic system delivers between 30 and 60 kN and how operators adjust the pressure for different materials, thicknesses, and joint geometries. The audit should also establish whether the dies and tooling supplied with the gun are suitable for the intended bracket design.
Request repeatability data rather than relying only on a single demonstration. The supplier should explain its method for selecting force settings, controlling joining depth, checking joint quality, and preventing damage to the workpiece. If your project includes high-strength steel, aluminum, coated sheet, or mixed-material assemblies, ask for relevant trial results and acceptance criteria.
Manufacturing Controls and Quality Documentation
Trace the complete production route from incoming materials and purchased components to machining, hydraulic assembly, electrical installation, tooling setup, calibration, functional testing, packaging, and shipment approval. The company states that it conducts full inspection throughout production and performs functional tests before delivery. During the audit, request sample records for the exact model and configuration you intend to purchase.
Important documents may include incoming inspection reports, assembly checklists, pressure or force test results, calibration records, final inspection forms, serial-number traceability, and release approvals. Test videos can also help confirm that the delivered tool configuration has been evaluated under practical operating conditions.
Engineering, Customization, and Application Experience
Assess whether the R&D team can support more than a standard catalog transaction. Questions should cover structural engineering, hydraulic development, motor systems, electrical controls, embedded software, prototype construction, reliability verification, tooling modification, and process validation. Questok reports experience with battery-powered hydraulic riveting tools, self-piercing riveting systems, SPR equipment, clinching tools, and integrated fastener assembly solutions.
Application references should be compared with your own production environment. In HVAC work, the supplier describes joining applications for ducts, fans, dampers, filters, and flanges, with benefits such as one-step operation, no consumables, and no polishing or repainting. It also reports self-piercing riveting and fastener installation experience for EV battery trays and water cooling plates.
For complex projects, ask how the supplier manages trials and production launch. One reported automotive project required both self-piercing riveting and rivetless clinching for challenging combinations of high-strength materials. The described approach included repeated material trials, metallographic analysis, tooling adjustments, and documented process development. Evidence of this kind can indicate whether the manufacturer is capable of supporting validation and implementation after the order is placed.
Capacity, Delivery, Compliance, and Service Questions
| Audit Category | Evidence and Questions to Review |
|---|---|
| Force and joining performance | Can the factory demonstrate 30–60 kN output, accurate pressure regulation, stable repeatability, and tooling compatibility with the target materials and bracket geometry? |
| Production capacity | Can it produce more than 800 standard sets and 500 customized sets, with a stated three-day lead time for qualifying standard orders and 15 days for customized solutions? |
| Quality assurance | Are materials, assemblies, pressure settings, calibration, finished products, and functional performance inspected and recorded? |
| Engineering support | Can the technical team perform prototypes, joining trials, reliability checks, metallographic evaluation, tooling changes, and production-transfer support? |
| Compliance and service | Which certificates apply to the exact product version, and how are warranty, spare parts, repairs, training, and technical requests handled? |
Certification and Commercial Due Diligence
The supplied records include CE certificates ISETC.001120210222 and 3N210218.PTK0S25, as well as an MSDS record numbered 262620110732. During the audit, confirm the scope and validity of each document. The certificate should correspond to the actual press tool configuration, production version, accessories, and destination market rather than only to a similar product family.
Commercial terms should also be documented before approval. Check the minimum order quantity of one set, standard and customized lead times, ODM and OBM arrangements, packaging responsibilities, spare-parts availability, warranty coverage, repair procedures, operator training, and the promised global technical response within 24 hours.
Frequently Asked Questions
Which factory records should be reviewed?
Ask to see incoming-material inspection, component and assembly records, force or pressure test data, calibration information, functional inspection reports, final release documents, and traceability records for the specific tool configuration.
How can I assess customization capability?
Request examples of prototype development, material-combination trials, die or tooling revisions, joining validation, and production implementation. Confirm the development schedule, test responsibilities, acceptance standards, and documentation required before approval.
What service conditions should be confirmed in the contract?
Verify the one-set MOQ, three-day standard delivery, 15-day customized delivery, inspection coverage, 24-hour technical response, warranty terms, replacement parts, repair handling, training, and the responsibilities of both supplier and buyer.
Conclusion
A successful factory audit should connect the press tool’s performance with objective evidence of process control, engineering depth, capacity, compliance, delivery reliability, and long-term service. For the QUESTOK rivetless clinching gun, verify the 30–60 kN force range, precise adjustment, tooling suitability, full inspection process, and performance on your actual joining application. The supplier supports ODM and OBM cooperation, accepts orders from one set, and reports experience in automotive, HVAC, aerospace, white goods, solar, and EV battery applications. For technical solutions or further support, please contact jane@questok.com.
About PHOTON TECHNOLOGY KUNSHAN CO.,LTD
PHOTON TECHNOLOGY KUNSHAN CO.,LTD, also known as Questok, develops fastening, joining, and assembly technologies for industrial manufacturing. Its product range includes battery-powered hydraulic riveting guns, SPR riveting systems, self-piercing riveting guns, clinching equipment, fasteners pressing tools, and integrated fasteners assembly solutions. Founded in 2011, the company operates a 5,000 sqm facility and reports capacity for more than 800 standard sets and 500 customized sets. Its supplied records include CE certifications and an MSDS, and its solutions serve customers in several manufacturing sectors.
REPORT