




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How Can Sample Trials Verify Mass Production Packaging Performance?
The most reliable way to determine whether sample results will represent mass production is to test the actual wafer product on the complete automatic packaging line. The trial should use the intended packaging film, stacking arrangement, product recipe, and downstream equipment. Record sealing performance, pack dimensions, production speed, rejection responses, film registration, and changeover parameters, then compare the findings with sample inspection results before approving delivery or production.
Mass Production Validation Strategy
A representative trial should follow the same route that products will take during normal operation. This includes feeding, alignment, stacking, film forming, longitudinal sealing, cross sealing, cutting, discharge, inspection, and any planned secondary packaging. Testing only the flow-wrapper section may overlook problems caused by product spacing, orientation, upstream accumulation, or downstream transfers.
Use the Intended Product and Packaging Format
- Run the actual wafer biscuits, wafer bars, creamed wafers, sandwich wafers, or chocolate-coated wafers planned for production.
- Maintain the production dimensions, filling or coating condition, orientation, stacking quantity, and pack configuration during the trial.
- Use the specified heat-sealable film and record film tension, reel setup, sealing temperatures, registration, and cutting performance.
- Evaluate fin seals, end seals, package length, product presence, reject accuracy, and repeatability over a sustained operating period.
- For high-volume facilities, include optional checkweighing, metal detection, gas flushing, labeling, cartoning, or robotic palletizing where these modules are part of the final line.
How the Wafer Packaging Process Affects Results
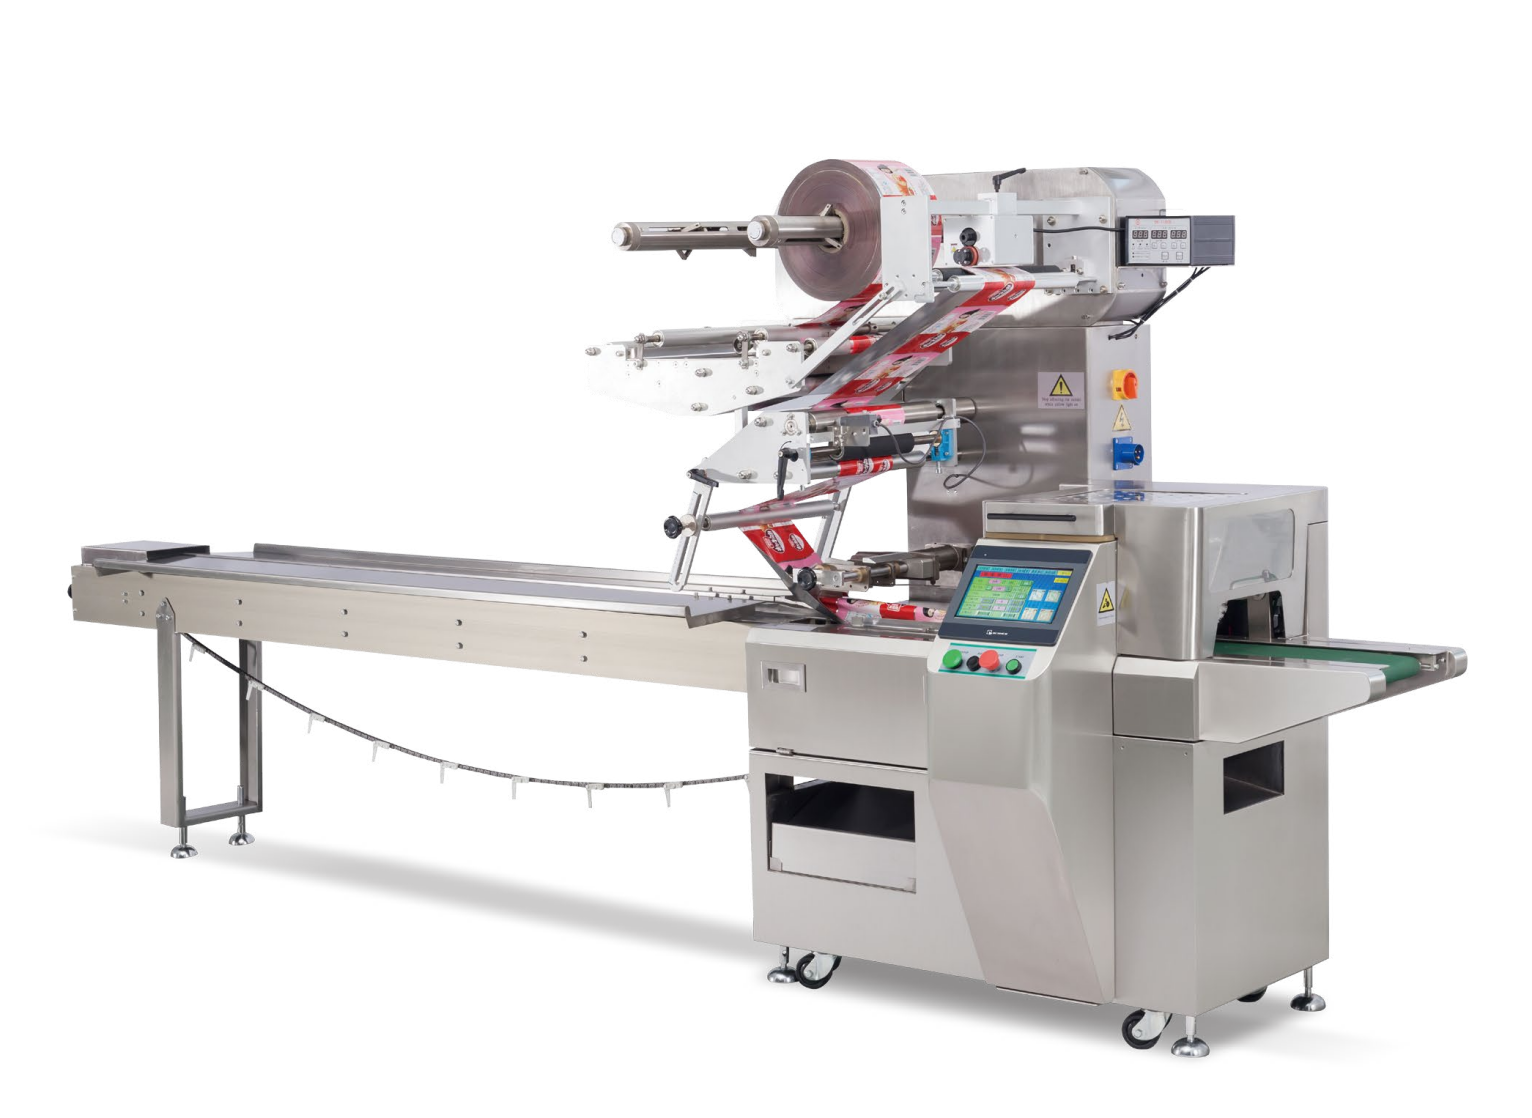
A horizontal wafer packaging line normally begins with conveyor feeding and product alignment. Products are then arranged or stacked before entering the film-forming section. The wrapper creates a longitudinal fin seal, forms cross seals, cuts individual packs, and transfers finished products to the next stage. Reproducing this complete process during sample testing gives a more accurate indication of production behavior.
Product characteristics should be fixed before the equipment is tested. The system can be configured for wafer biscuits, wafer bars, creamed wafers, sandwich wafers, and chocolate-coated wafers. With an optional collating unit, automatic stacking may prepare two to six wafers per package. Photoelectric sensors monitor product position, while multi-lane arrangements can be selected when a higher output level is required.
Film, Sealing, and Registration Checks
The film used for validation should be the same material intended for commercial operation. Suitable structures may include OPP, CPP, PET/Alu/PE, or metallized heat-sealable film. During the trial, operators should inspect film tracking, tension stability, fin-seal appearance, cross-seal strength, cut-off quality, and printed design alignment. Color-mark tracking is available with stated accuracy of plus or minus 1 mm, but the achieved result should still be confirmed with the selected film and artwork.
Each test should be linked to a clearly identified machine recipe. PLC-based control, distributed servo drives, a color touchscreen, recipe storage, alarm records, and diagnostic functions help preserve the tested settings. Depending on the model, the machine may use three servo axes, four servo axes, or a full-servo configuration. The report should document infeed speed, film-feed values, sealing parameters, product arrangement, and any adjustments made during operation.
Measurements to Record Before Approval
Finished packages should be checked for dimensional consistency, correct product loading, seal integrity, registration accuracy, and clean cutting. Where required, automatic rejection should be verified for missing products, defective seals, incorrect weight, or other identified faults. The line may also connect with a checkweigher, metal detector, labeler, cartoner, or robotic palletizer, so each transfer point should be observed during the trial.
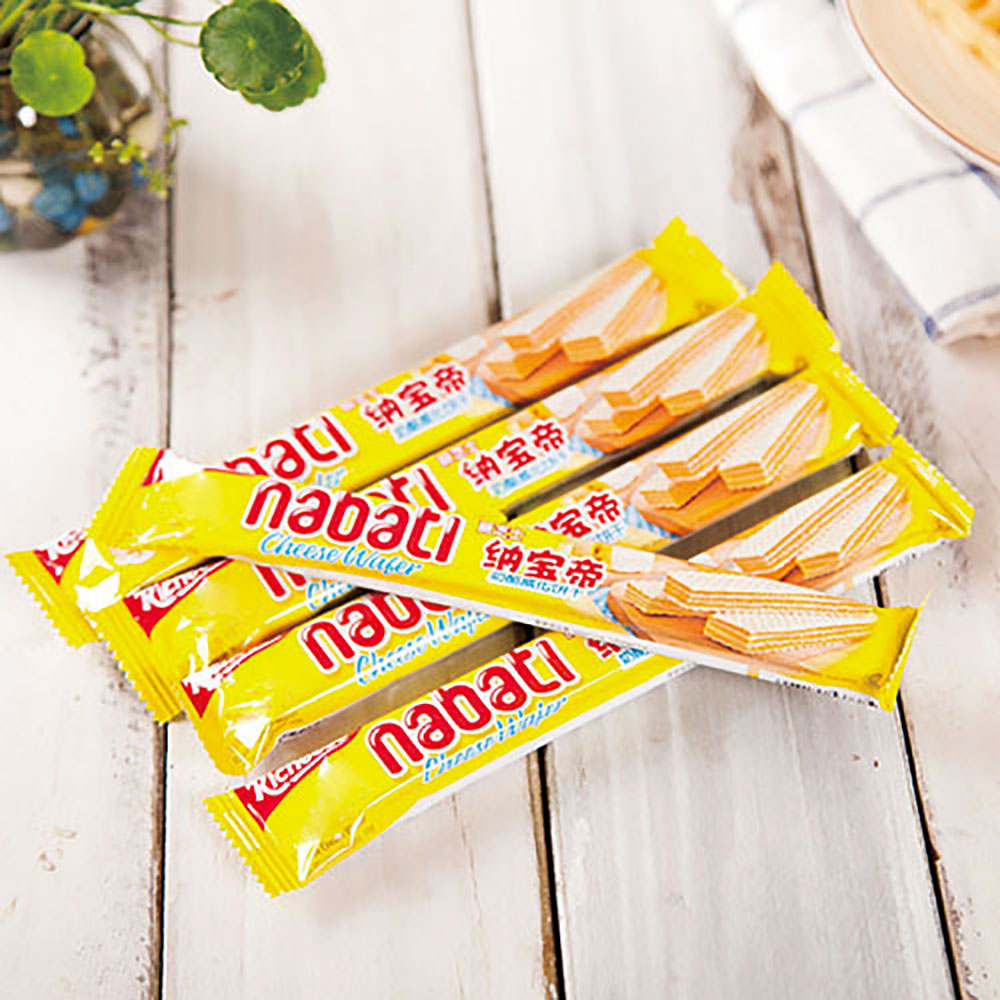
Recorded output must be interpreted according to the tested machine class and product configuration. Entry-level, mid-range, and high-speed full-servo models may offer different operating ranges. The stated capacity is not a universal guarantee because product dimensions, film construction, pack length, stacking method, and packaging format all influence actual throughput. A valid sample report therefore identifies the precise conditions under which each result was obtained.
Validation Data Comparison
| Validation Item | Trial Evidence to Review | Applicable Equipment or Data |
|---|---|---|
| Feeding and product handling | Consistent spacing, orientation, stacking, and transfer into the wrapper | Belt conveyor, vibratory alignment, photoelectric sensors, and optional two-to-six-wafer stacking |
| Film and sealing | Stable fin seals, cross seals, cutting, and printed-film alignment | Heat-sealable laminates, preheating assembly, heated jaws, and color-mark tracking |
| Throughput | Repeatable output using the approved product and pack format | Typical capacity of 100 to 1,000 packs per minute, subject to product and film conditions |
| Finished-pack quality | Correct dimensions, product presence, seal condition, and rejection response | Automatic defective-pack ejection and typical pack lengths of 60 to 300 mm, depending on the product |
| Line integration | Reliable movement into inspection, secondary packaging, and palletizing equipment | Optional checkweigher, metal detector, labeler, cartoner, and robotic palletizer |
| Recipe repeatability | Ability to restore the approved settings during future production | PLC control, touchscreen recipes, fault records, and remote diagnostic functions |
Frequently Asked Questions
What product is appropriate for the sample test?
The trial should use the exact wafer product planned for production, including its dimensions, coating, filling, stacking quantity, and orientation. A substitute product may feed differently, require other sealing conditions, or produce a different achievable speed.
What should be confirmed about the packaging film?
Use the intended heat-sealable laminate and document its width, reel installation, tension, longitudinal seal, cross seal, cutting behavior, and printed registration. Film material and packaging format have a direct effect on the final result.
Does a sample trial prove the machine's maximum rated speed?
The trial establishes performance for the tested configuration rather than guaranteeing the highest published speed. Flow-wrapping modules may operate across ranges such as 30 to 250 packs per minute, with selected servo models offering higher performance. Actual output depends on the product, film, pack dimensions, and operating recipe.
Conclusion and Recommended Approval Process
Before confirming mass-production readiness, test the complete wafer packaging route with the real product, film, stacking pattern, machine recipe, and planned line extensions. Retain measurements for throughput, package dimensions, seal quality, registration, product presence, reject accuracy, and changeover recovery. These records provide a practical reference for production acceptance and future troubleshooting.
Foshan Ruipuhua Machinery Equipment Co. Ltd supports equipment manufacturing, OEM cooperation, sample trials, and engineering assistance for automated packaging projects. Its R&D scope includes product testing, PLC and HMI integration, film handling, and synchronized packaging lines. The company states that its CE certification covers flow packaging machines, automatic packaging systems, cartoning machines, and palletizing robots. A documented chocolate pie cake project supplied 27 sets for a major bakery manufacturer operating across Vietnam, Korea, and China, combining forming, baking, filling, chocolate enrobing, wrapping, and robotic palletizing.
For technical consultation or sample-based packaging support, contact lotuspack@ruipuhua.com.
About Us
Foshan Ruipuhua Machinery Equipment Co. Ltd develops and manufactures intelligent packaging machinery, providing R&D, production, installation, and technical after-sales service. Established in 2005, the company operates a manufacturing facility with an annual capacity of more than 500 automatic packaging machines and complete packaging lines. Its solutions are used in food, bakery, biscuit, snack, noodle, chocolate, soap, hardware, pharmaceutical, and daily chemical applications in more than 100 countries.
The company holds CE certification for flow packaging machines, automatic packaging systems, cartoning machines, and palletizing robots, and has supplied automated equipment for customers in a range of industries.
REPORT