




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Control Compliance Risks in Two-Plastic Injection Molded Parts
Using two different plastics in a single molded component can introduce compliance issues if the materials, mold design, inspection criteria, or production changes are not formally controlled. The main risks include incompatible resin specifications, an unsuitable cavity or runner layout, dimensional instability, incomplete quality records, and unauthorized modifications to a double-shot or overmolding process.
Primary Compliance Controls
Before tooling starts, document the complete product and manufacturing requirements. This should include the exact resin grades, material pairing, processing temperatures, mold structure, runner system, molding sequence, tolerances, surface expectations, and inspection responsibilities.
- Confirm whether the part will use a cold-runner or hot-runner system and whether the process is double-shot molding or overmolding.
- Approve mold trial results, production samples, dimensional reports, surface checks, and pre-shipment inspection records before releasing the tool for regular production.
- Verify that the selected mold base, cavity steel, tolerance level, and projected mold life are suitable for the approved part requirements.
- Apply application-specific review to components for consumer electronics, household appliances, automotive systems, industrial equipment, and everyday consumer products.
Material and Mold Design Review
A two-plastic part should not be approved solely because both materials are commonly used in injection molding. The supplier and buyer need to validate the specific resin combination, including adhesion, shrinkage, temperature compatibility, chemical resistance, and the order in which the materials will be molded. The available tooling supports cold-runner and hot-runner designs, but those options do not establish a universal material combination for every application.
The mold architecture must also correspond to the product geometry and the selected process. Important review points include cavity alignment, parting surfaces, mold base selection, cavity steel, runner balance, insert positioning, and the dimensional control of features formed by each plastic. For higher-precision tools, CMM measurement, surface inspection, and repeated mold trials can provide evidence that the design performs consistently.
Validation, Records, and Change Control
Production approval should rely on documented physical results rather than a notice that mold construction has been completed. A suitable validation package may include mold trial reports, first article inspection, full dimensional measurement, sample approval, mold running tests, surface-quality records, and multi-cycle trials. These records help demonstrate whether the approved sample matches parts produced later.
Any change to resin grade, molding sequence, runner configuration, processing conditions, cavity components, or inspection method should be reviewed through a defined change-control process. This is particularly important for double-shot and overmolded components, where a small change can affect alignment, bonding, appearance, shrinkage, or assembly performance.
The listed tooling specification gives a precision tolerance of ±0.02 mm and a mold life range from 50,000 to 1,000,000 shots. These figures should be checked against the customer's drawings, functional requirements, and approval documents. They should not be treated as automatic performance guarantees for every two-material mold.
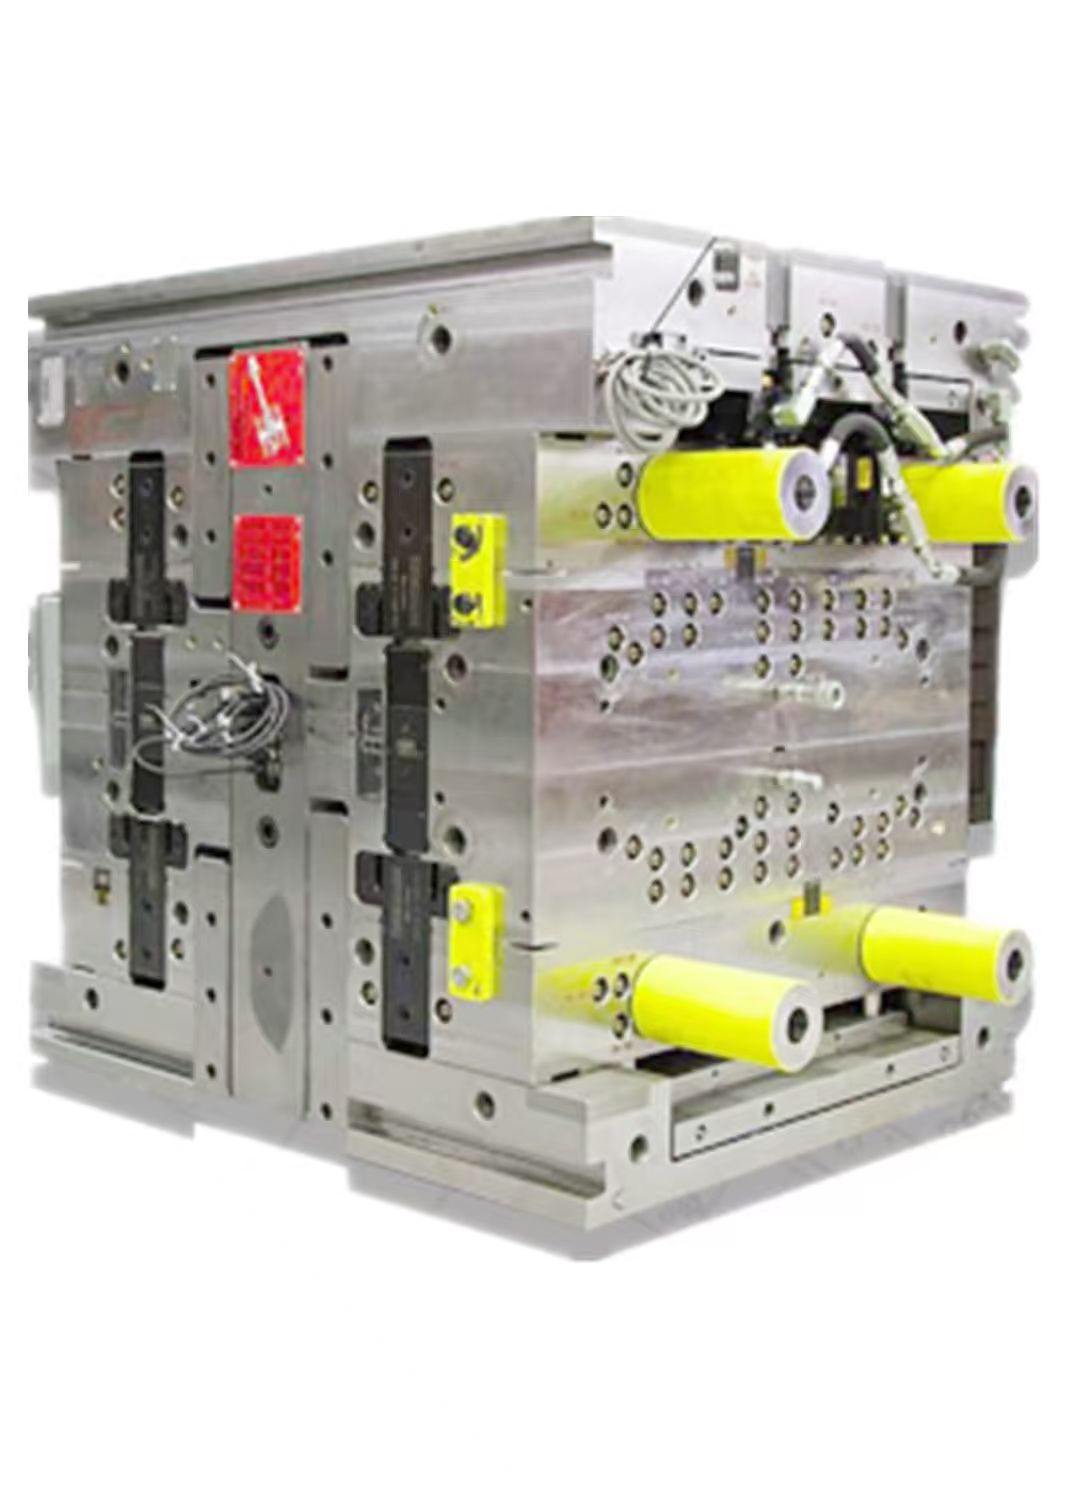
Compliance Checkpoint Comparison
| Review area | Control to confirm |
|---|---|
| Materials and process | Approve the two resin grades, molding sequence, double-shot or overmolding method, and cold-runner or hot-runner arrangement. |
| Tool construction | Available options include S50C or P20 mold bases and 718H, 1.2738, or S136 cavity steels. |
| Dimensional quality | Verify the stated ±0.02 mm precision requirement through dimensional inspection, full measurement, and CMM testing where required. |
| Process qualification | Use mold trials, running tests, sample confirmation, and multi-cycle testing to assess repeatability. |
| Release before shipment | Complete the agreed pre-shipment full inspection or applicable IQC, IPQC, and FQC controls, with sample sign-off where required. |
| Ongoing support | Confirm access to technical assistance, maintenance guidance, spare parts, and future mold optimization support. |
Relevant Manufacturing Experience
Longterm Mold has reported experience producing double-shot overmolding tools for a French product brand. One project included eight mold sets for a consumer electronics shell, with customer feedback noting good alignment and stable trial samples. Reported applications also include electronic housings, home appliance components, and industrial equipment enclosures.
The company states that it holds ISO 9001:2015 certification covering the design, manufacture, and sale of precision molds, as well as the sale of plastic products. Certification can support a structured quality system, but project-specific material approvals, inspection evidence, and change records still need to be reviewed for each product.
Frequently Asked Questions
What must be approved before manufacturing a two-material mold?
Approve the precise resin grades, compatibility requirements, part drawings, tolerances, molding process, runner design, inspection plan, trial-sample acceptance criteria, and procedures for controlling later changes. The available tooling information identifies process choices but does not prescribe one material pairing for all projects.
Which inspections are useful for a double-shot molded component?
Depending on the product specification, useful controls include mold trial testing, first article inspection, CMM measurement, complete dimensional inspection, surface evaluation, multi-cycle trials, mold running tests, sample confirmation, and pre-shipment full inspection.
Can the same supplier handle tooling and injection production?
Yes. The listed service models include custom mold making with injection molding and mold development followed by plastic injection mass production. The latter states mold delivery in 25–35 days and mass production in 7–15 days after sample approval.
Conclusion
Compliance for a part made from two plastics depends on traceable control of the materials, mold architecture, process sequence, trial samples, dimensions, appearance, inspections, and production changes. The inspection scope should reflect the part's function, geometry, customer specification, and risk level. Sample approval should be completed before shipment whenever required.
Longterm supports OEM custom plastic injection molds, precision double-shot and overmolding tools, custom mold making with injection molding, and mold development combined with mass production. For technical consultation, contact rogerluo@longterm-mold.com.
About Us
Longterm Manufacturing Solutions Limited was established in 2010 and supplies mold design, tooling, precision machining, mold manufacturing, and plastic parts production to customers in North America, Europe, Australia, and other international markets. The company has 50 employees, including a five-person R&D team focused on mold engineering and precision machining. Its capabilities include injection-mold structural design, CNC component production, sample validation, and process improvement. The company reports ISO 9001:2015 certification and experience serving customers across several industries.
REPORT