




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Verify a Rectangular Clinching Gun Fits Your Panels
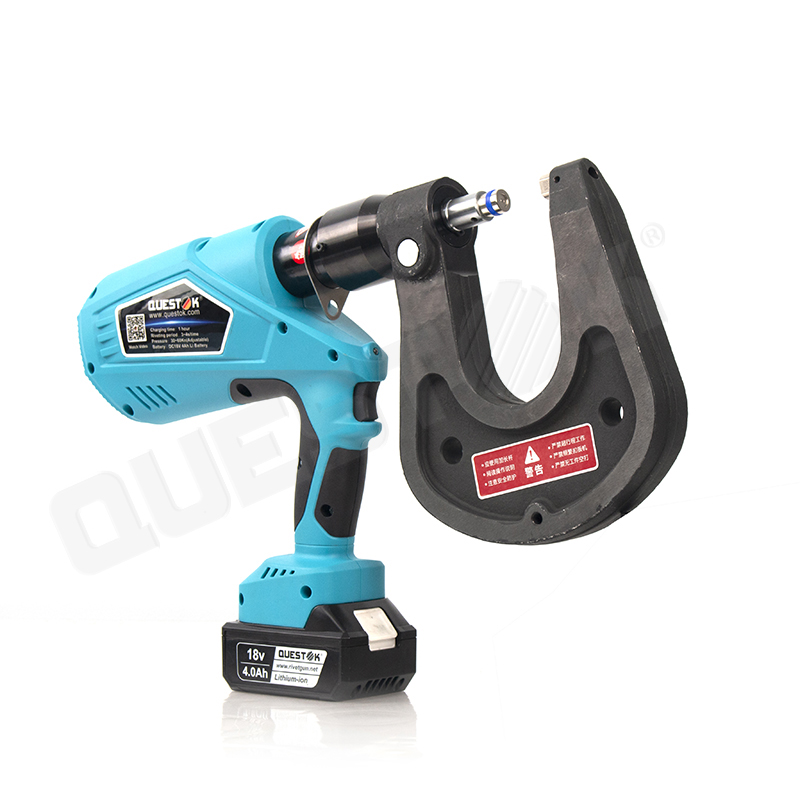
Determining whether a rectangular clinching gun is suitable for your panels requires more than checking the tool’s shape. You should review the panel materials, thickness combination, joint requirements, access to each joining point, and the force needed to form the joint. Questok’s rectangular clinching gun for elevator cabins provides an output pressure of 30–60 kN, but sample joining tests are recommended before the equipment is introduced into regular production.
Compatibility Review: What to Check First
- Identify the intended application and the materials being joined.
- Confirm the combined panel thickness and the required clinch joint design.
- Compare the estimated forming demand with the tool’s 30–60 kN output pressure.
- Verify that the gun can access every planned joining location.
- Inspect the finished joint for strength, appearance, and dimensional requirements.
How Rectangular Clinching Compatibility Is Determined
A rectangular clinching gun creates a mechanical sheet metal joint by locally forming and interlocking the panels. Its suitability depends on the complete joining process, not simply on the dimensions or outline of the workpiece. Material type, sheet thickness, joint position, die configuration, throat depth, access limitations, and required joint quality should be assessed together.
The Questok model is designed for elevator cabin panel applications and has a stated output pressure of 30–60 kN. This range provides an initial reference for evaluating the available forming force. However, the supplied product information does not specify universal limits for panel thickness, die size, throat depth, or joint geometry. These technical details should therefore be verified through an application assessment using the customer’s actual panels.
Applications and Practical Testing
Questok lists sheet metal joining experience in HVAC ductwork, air fans, dampers, filters, and flanges. Its rectangular clinching solutions are also used for stainless steel components in white goods, commercial kitchens, and commercial freezers. These examples show where the technology may be relevant, but they do not replace a test with the specific material combination, panel geometry, and production conditions involved in a new project.

A suitable evaluation should include representative samples and the intended joint locations. Engineers can then check whether the tool reaches the work area, whether the available force forms the joint correctly, and whether the finished connection meets strength and visual standards. This approach is especially important when panels contain stainless steel, multiple layers, narrow flanges, or difficult-to-reach areas.
Engineering Support and Production Experience
Questok’s development capabilities include mechanical design, hydraulic system engineering, structural analysis, electrical controls, fastening process development, prototype trials, reliability verification, and application engineering. These resources support a compatibility review based on the customer’s panels instead of relying only on general product specifications.
In a reported Midea control cabinet project, Questok provided a clinching solution that improved work efficiency and reduced production costs compared with welding. The process used a single joining operation without consumables, polishing, or repainting. A separate elevator cabin application should still be tested independently because its materials, thicknesses, geometry, and access conditions may be different.
Product Data for an Initial Fit Assessment
| Assessment Factor | Available Information |
|---|---|
| Typical target application | Elevator cabin panels, with related applications in HVAC, white goods, commercial kitchens, and commercial freezers. |
| Output pressure | 30–60 kN |
| Panel and joint limits | Material pairing, thickness range, die dimensions, throat depth, and joint geometry require technical confirmation. |
| Quality inspection | The product is fully inspected, and completed equipment is function-tested before delivery according to the company’s stated process. |
| Customization | Customization is available, with a stated 15-day customization lead time. |
Frequently Asked Questions
Which information is needed for a compatibility check?
Prepare the panel materials, individual and combined thicknesses, intended joining points, available working space, desired joint type, production volume, and quality requirements. Clear application data allows the tool and joining process to be evaluated accurately.
Will 30–60 kN work for every panel combination?
No. The 30–60 kN output pressure indicates the available force range, but actual suitability depends on the material pair, thickness combination, joint geometry, forming conditions, and access. A practical sample test is necessary before confirming the equipment.
Can the rectangular clinching gun be modified for a specific project?
Customization is supported. The product information states a 15-day customization period and a minimum order quantity of one set. Final technical requirements, tooling, and delivery details should be confirmed with the supplier.
Recommended Selection Process
Start by documenting the complete panel application, then compare the required joint conditions with the tool’s 30–60 kN output pressure. Next, confirm access, tooling dimensions, and joint appearance through representative samples. Only after the test results meet the required performance should the rectangular clinching gun be approved for production.
Questok supports ODM and OBM models, provides full product inspection, and accepts orders from one set. For application-specific technical guidance, contact jane@questok.com.
About Us
PHOTON TECHNOLOGY KUNSHAN CO., LTD, also known as Questok, is an industrial technology company developing fastening, joining, and assembly solutions for manufacturing. Founded in 2011, the company operates a 5,000 sqm facility and serves automotive, electric vehicle, transportation, sheet metal, appliance, electronics, construction, and general industrial markets. Its R&D activities include clinching equipment, clinching guns, SPR riveting systems, fastener pressing tools, process development, testing, and production integration. Questok holds CE and MSDS certifications and has supplied solutions for customers in multiple industries.
REPORT