




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Key Design Constraints for Complex Double Shot Molding Parts
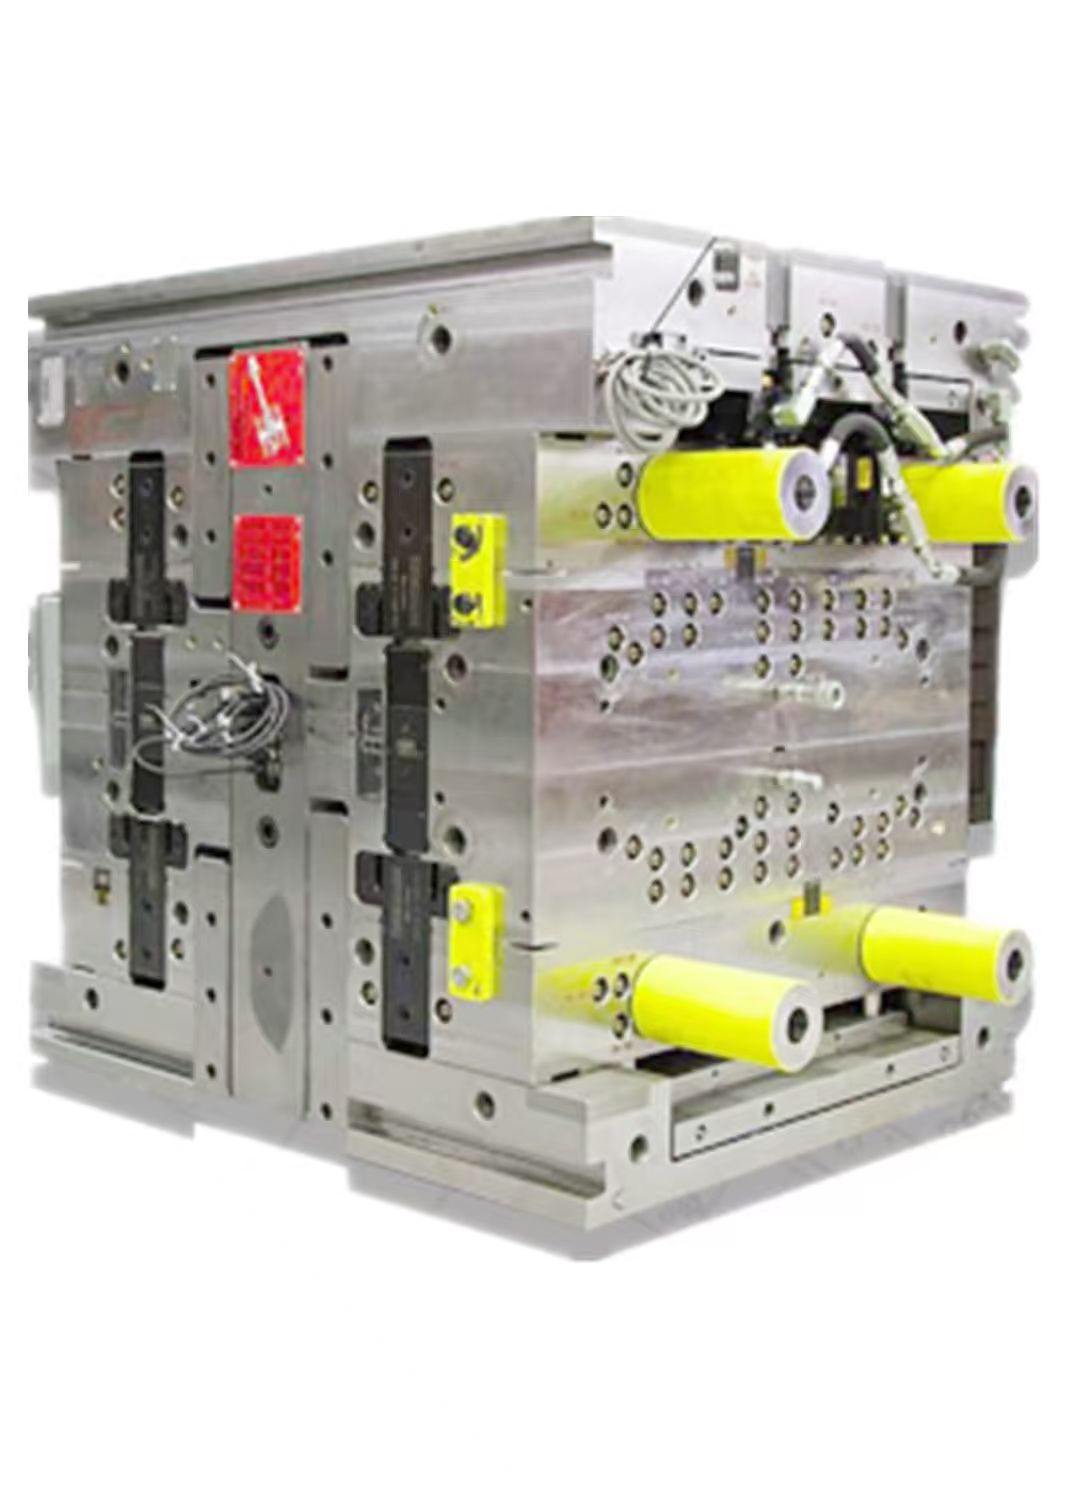
Designing a complex double shot molding part requires early decisions about part architecture, material compatibility, tooling steel, runner layout, dimensional control, inspection, and production timing. Before mold construction begins, confirm whether the component needs true two-shot molding or an overmolding process, define the material or color interface, and establish the approval criteria for samples and production.
Important Design Parameters
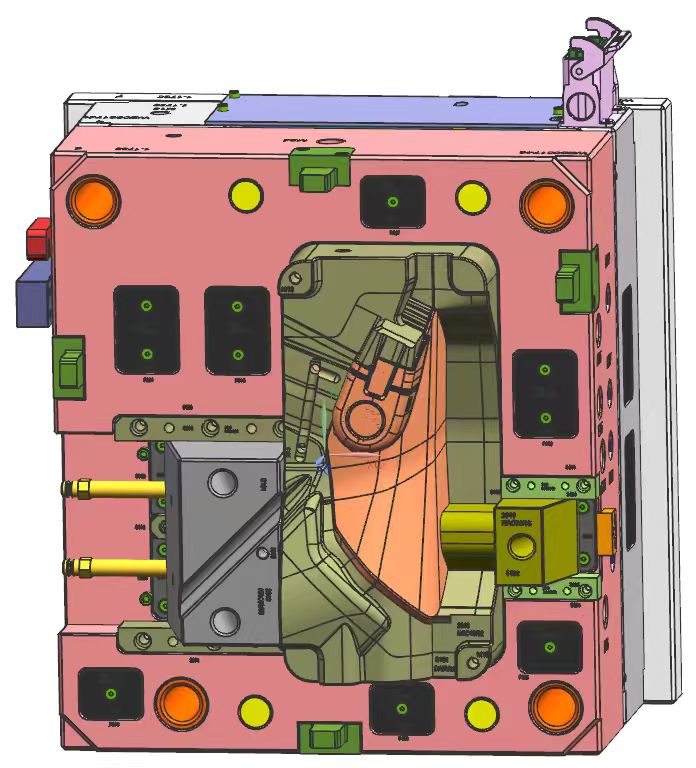
The practical limits of a double shot molding project depend on the part geometry and the interaction between its two molded sections. Engineering teams should define the molding sequence, registration features, bonding or mechanical interface, critical dimensions, surface expectations, and functional areas before finalizing the tool design.
Available tooling solutions include custom plastic injection molds for double shot and overmolding applications. However, the supplied specifications do not establish universal limits for part size, wall thickness, or every possible material combination. These factors must be reviewed against the selected resins, shrinkage behavior, molding temperature, required bond strength, and the finished part's geometry.
Tooling Materials and Runner Options
Material selection has a direct effect on tool durability, machining performance, surface quality, and maintenance requirements. The mold base can be manufactured from S50C or P20, while cavity steel options include 718H, 1.2738, and S136. S136 may be considered when corrosion resistance or a demanding surface finish is important, while other steel grades may be selected according to production volume and cost targets.
Both cold runner and hot runner systems are available. The best configuration depends on the approved mold layout, resin selection, gate location, cycle requirements, cosmetic standards, and expected production quantity. Runner selection should therefore be made as part of the complete mold design rather than treated as an isolated option.
Precision, Validation, and Mold Life
The stated dimensional capability for the custom plastic tooling product is ±0.02 mm. This figure should be applied only to dimensions that can be consistently measured under agreed inspection conditions. Double shot molds also require careful control of part transfer, alignment, shrinkage, and the interface between the first and second shots.
Validation may include mold trials, dimensional measurement, surface inspection, CMM testing, multi-cycle testing, and a complete pre-shipment inspection. Sample approval should be completed before mass production is scheduled. Depending on the material, tooling design, and maintenance program, the expected mold life is listed at 50,000 to 1,000,000 shots.
Schedule and Project Planning
Timing is another factor that limits customization decisions. General custom plastic injection tooling is quoted at approximately 25–40 days, while a complex precision double shot or overmold project is expected to require about 35–45 working days. Projects involving difficult alignment, multiple mold trials, tight tolerances, or extensive inspection should be planned around the longer range.
Mass production is normally arranged after trial parts have been evaluated and approved, so production scheduling should be separated from the initial tooling estimate. Providing complete 3D files, 2D drawings, material information, critical tolerances, appearance requirements, and inspection standards at the start can reduce avoidable design revisions.
Relevant Experience and Quality Control
Longterm Manufacturing Solutions Limited reports experience with comparable tooling programs. One French consumer electronics customer commissioned eight sets of double shot overmolding molds, with reported results including accurate alignment and stable trial samples. Additional projects have included electronic housings for an Italian manufacturer, household appliance components for a United States distributor, and industrial equipment housings for an Australian customer.
The company is certified to ISO 9001:2015 under certificate number 02825Q12549R0S. The certification covers the design, manufacture, and sale of precision molds, together with the sale of plastic products. Its listed quality activities provide a structured reference for tooling checks, sample validation, and shipment approval.
Specification Overview
| Project consideration | Available information |
|---|---|
| Mold base and cavity steel | S50C or P20 mold base; 718H, 1.2738, or S136 cavity steel |
| Runner system | Cold runner or hot runner configuration |
| Stated dimensional tolerance | ±0.02 mm for the custom plastic tooling product |
| Projected mold service life | Approximately 50,000–1,000,000 shots |
| Complex tooling schedule | About 35–45 working days for a complex precision mold |
| Validation and inspection | CMM measurement, surface checks, mold trials, dimensional inspection, and pre-shipment inspection as required |
Frequently Asked Questions
Which details should be settled before tooling starts?
Confirm the two-shot or overmolding method, molding sequence, material or color pairing, interface design, critical dimensions, cavity steel, runner style, inspection requirements, and sample approval process. Part size, wall thickness, and resin compatibility are not covered by a universal published limit and require engineering evaluation.
Is a hot runner available for double shot tooling?
Yes. The listed tooling service supports either cold runner or hot runner systems. The final choice should follow the approved part design, materials, gate strategy, cycle requirements, and production plan.
What lead time should be allowed?
For a complex precision double shot or overmolding mold, the stated planning range is 35–45 working days. Standard custom plastic tooling is listed at 25–40 days, but the confirmed schedule depends on design complexity, trial requirements, revisions, and approval timing.
Practical Recommendations
Build the design around a clearly defined two-shot structure and review material compatibility before releasing the mold. Select steel and runner systems according to service life, appearance, volume, and maintenance needs. Apply the ±0.02 mm capability only where inspection conditions support it, and include trial molding, dimensional verification, surface checks, and sample approval in the project schedule.
Longterm supports OEM custom plastic injection molds, mold making with injection molding, precision double shot and overmold tooling, and mold development linked to mass production. For technical consultation, contact rogerluo@longterm-mold.com.
About Longterm Manufacturing Solutions Limited
Longterm Manufacturing Solutions Limited was founded in 2010 and serves customers in the United States, Europe, Australia, and other international markets. Its capabilities cover mold design, precision machining, tooling production, mold manufacturing, and plastic part production. Five R&D engineers use UG, SolidWorks, and AutoCAD to support mold structure design, CNC component development, sample verification, and process improvement. The company holds ISO 9001:2015 certification and has completed projects for customers in several industrial sectors.
REPORT