




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Selecting the Right Self-Piercing Riveting (SPR) System for Automotive Body Fabrication
Understanding Self-Piercing Riveting in Vehicle Assembly
Self-piercing riveting (SPR) has emerged as a crucial cold mechanical joining technology for modern vehicle manufacturing. Unlike traditional spot welding, the SPR technique penetrates the upper sheet layer and flares the semi-tubular rivet shank into the lower layer within a specialized die cavity. This process forms a robust mechanical interlock without thermal input, preserving protective anti-corrosion coatings and eliminating heat deformation across galvanized steel and lightweight aluminum body components.
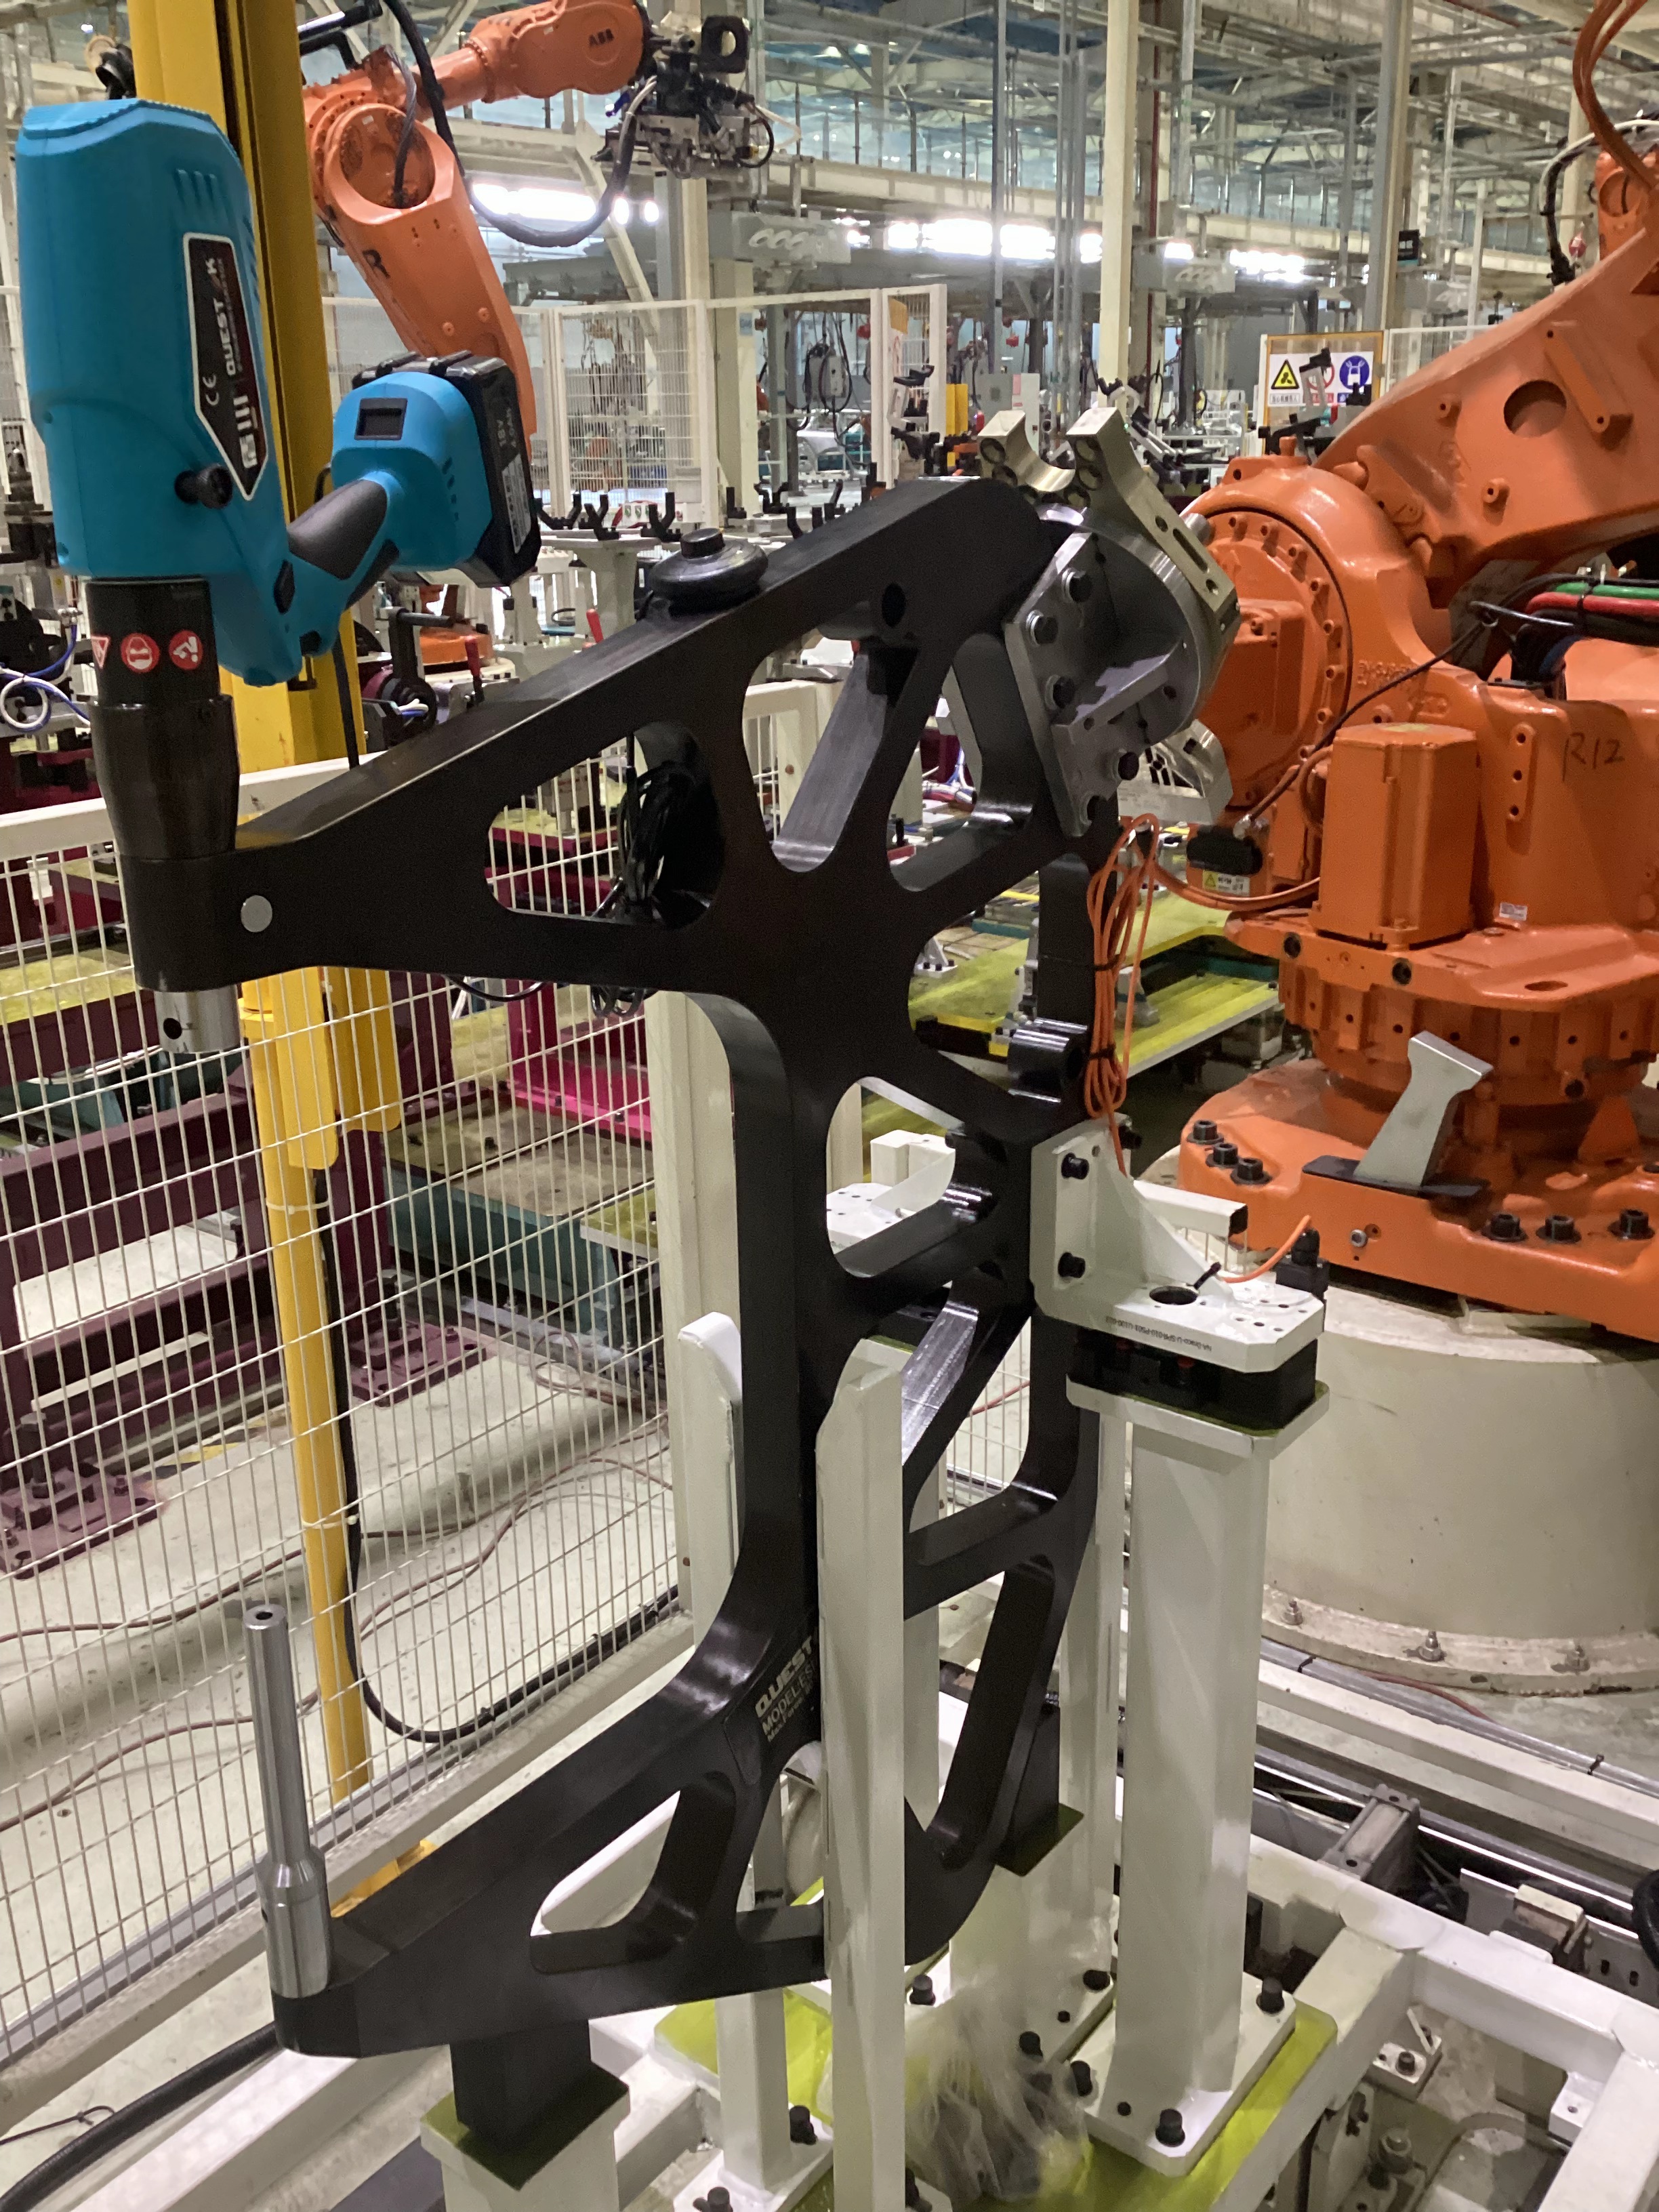
Whether assembling outer body skins, structural Body-in-White (BIW) modules, or EV battery housing systems, selecting the appropriate SPR equipment depends on aligning hydraulic output force, C-frame accessibility, and die configurations with your specific stack-up requirements.
Key Factors When Choosing an Automotive SPR System
- Precise Stepless Pressure Regulation: Equipment with variable setting ranges from 1 to 80 kN allows exact matching to material hardness, preventing outer panel surface damage or under-setting issues.
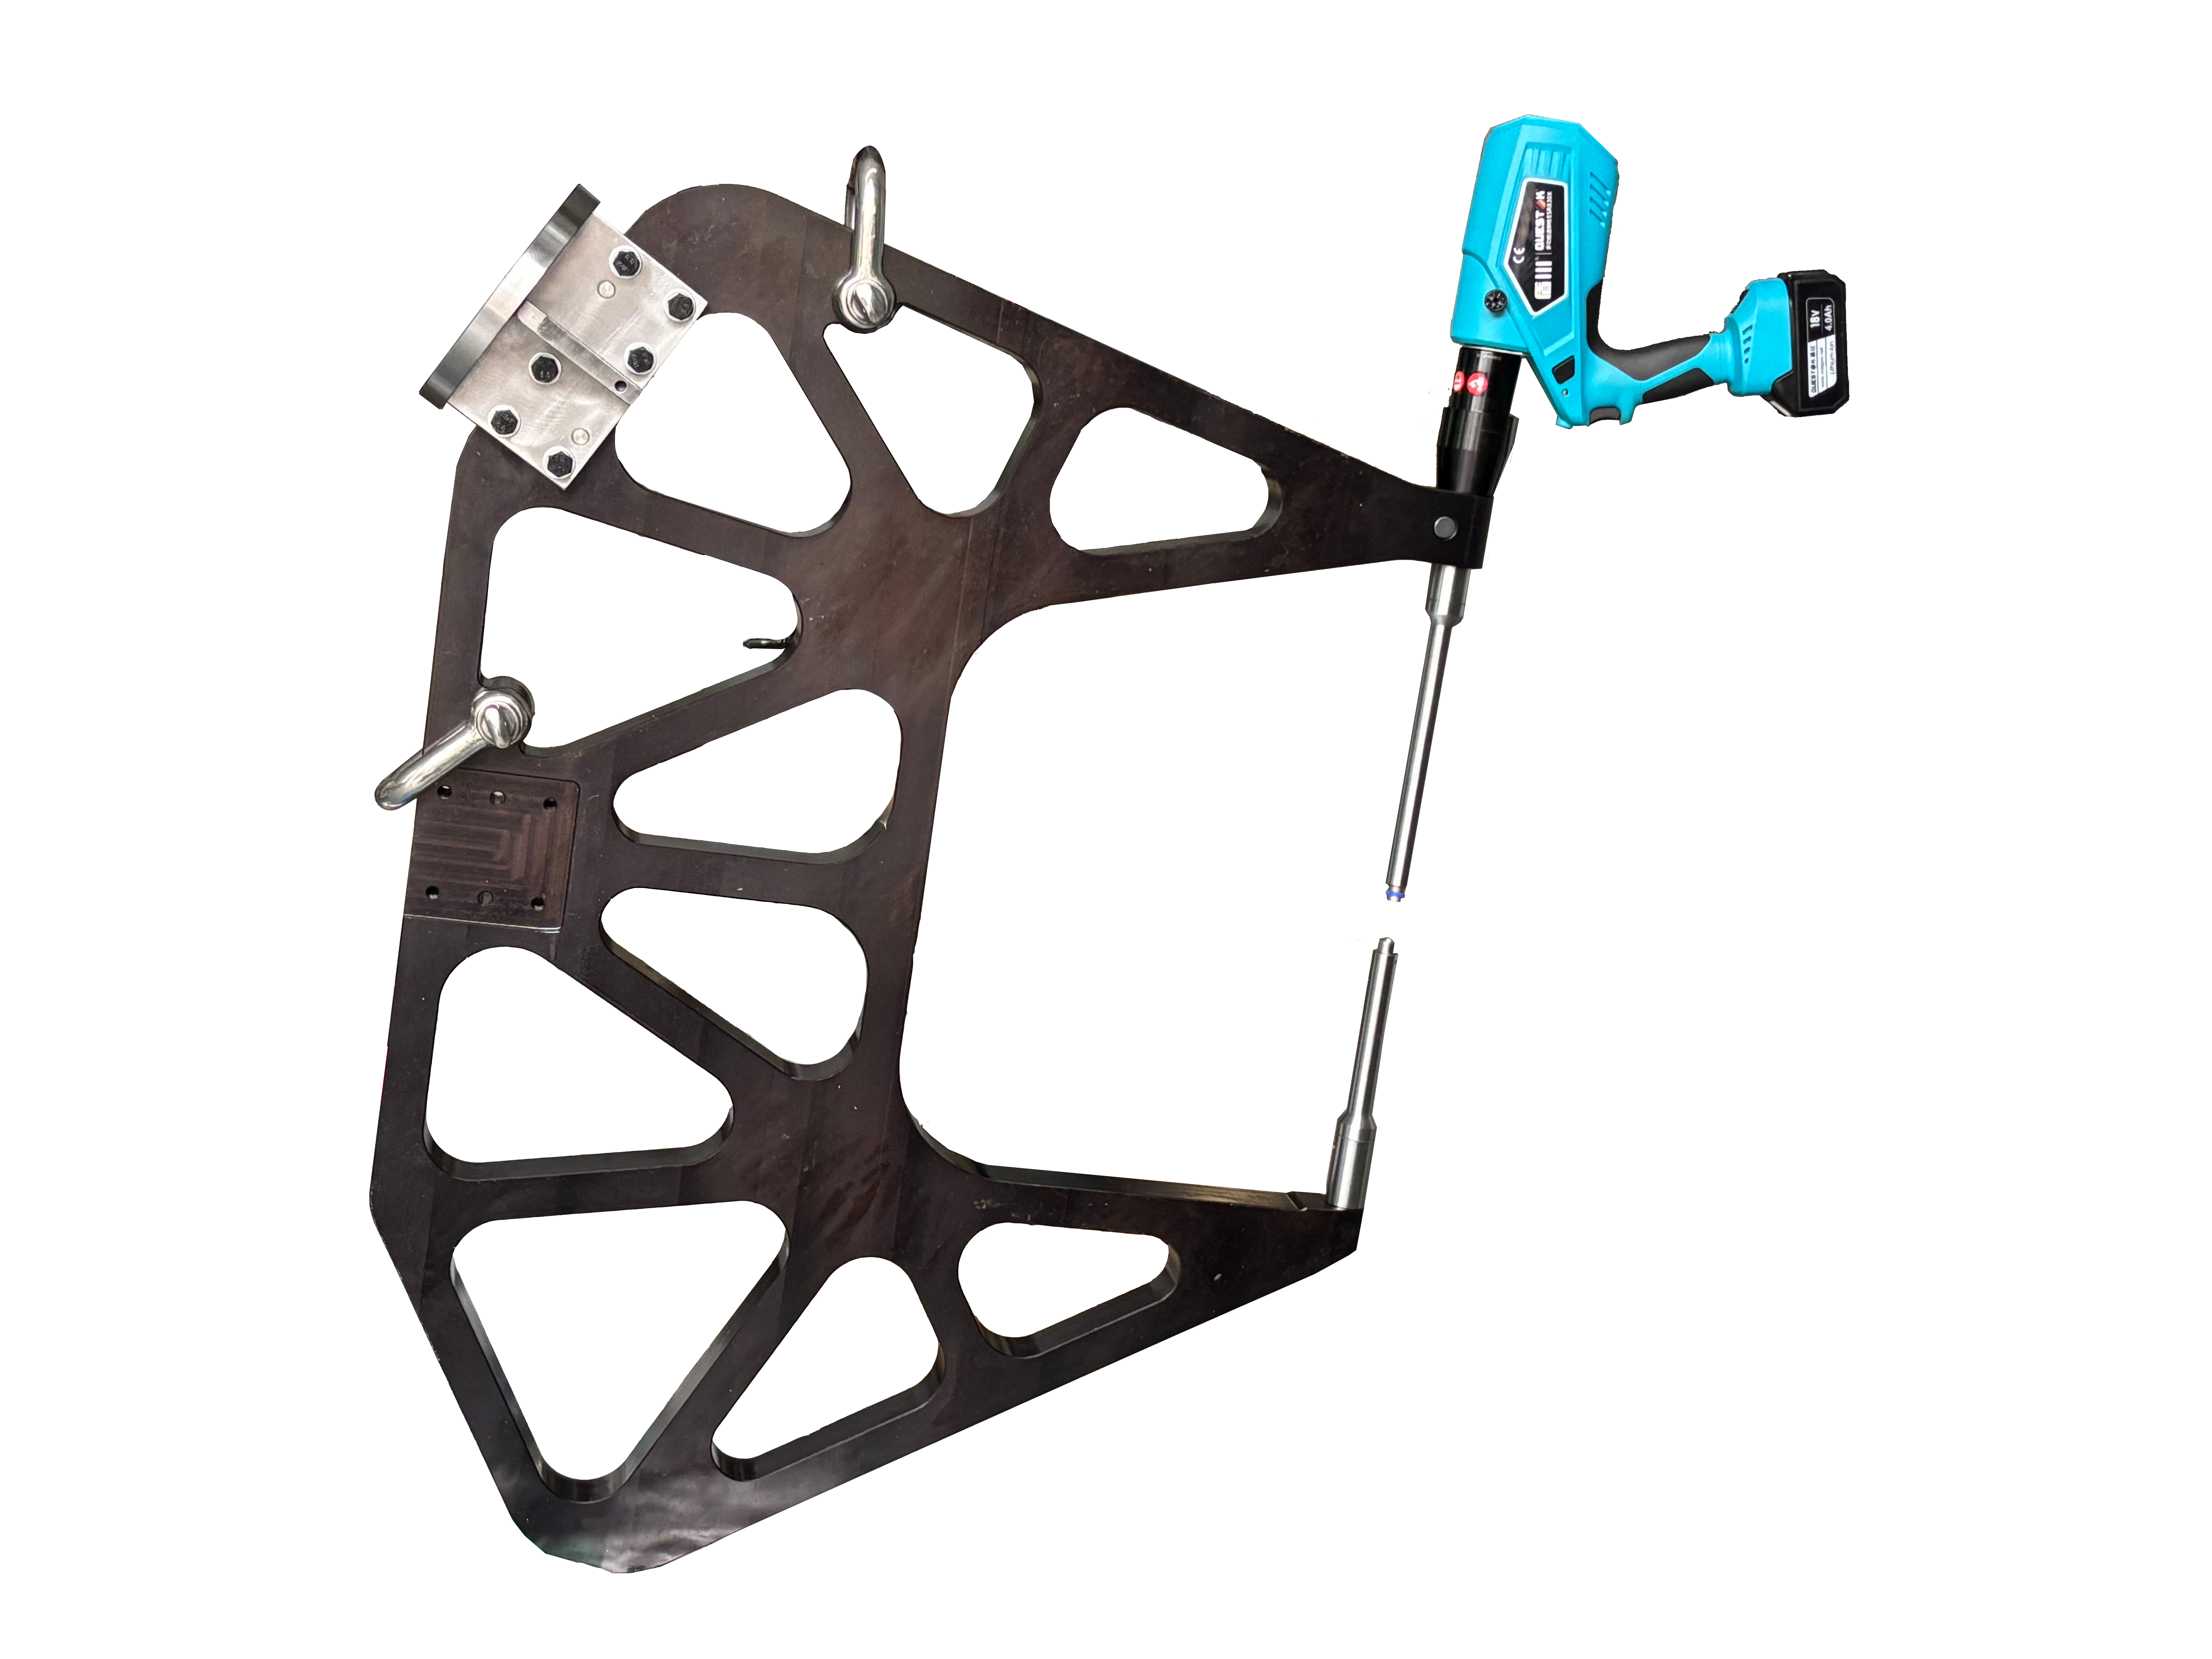
- Optimized Frame Geometry: Flexible C-frame reach and stroke options ensure unhindered tool maneuverability around complex geometries like wheel arches, door frames, and structural pillars.
- Multi-Material Compatibility: High-performance rivet-and-die sets enable direct joining of high-strength aluminum alloys to steel sheets without hole pre-punching.
- Rigorous Quality Assurance: Proven operational reliability with 100% full inspection and compliance with international CE and MSDS standards.
Application Breakdown and Equipment Technical Matrix
Modern auto manufacturing spans thin 0.8 mm external skins to multi-layer 3.0 mm structural alloys. Leading OEMs and battery producers—including Mercedes-Benz (Fuzhou), SAIC, NIO, CATL, and BYD—utilize hydraulic pressure control to ensure complete interlock without piercing bottom sheets or compromising liquid-tight seals in battery cooling plates.
| Application Type | Joined Materials | Target Force Range | Recommended Tooling | Delivery Timeline |
|---|---|---|---|---|
| Exterior Closures & Body Skins | Aluminum / Galvanized Steel (1.0 – 2.5 mm) | 10 – 35 kN | Portable Battery-Hydraulic SPR Unit | 3 Days (< 50 sets standard) |
| BIW Joints & Wheel Arch Prototypes | High-Strength Aluminum (2.0 – 5.0 mm) | 35 – 80 kN | High-Pressure Adjustable SPR Assembly | 15 Days (Customized Setup) |
| EV Battery Enclosures & Cooling Plates | Multi-layered Aluminum & Stainless Steel | 40 – 80 kN | Integrated Automated Riveting Platform | 15 Days (Customized Setup) |
Frequently Asked Questions
Q: Why is stepless force control essential for varying joint thicknesses?
A: Maintaining exact hydraulic control between 1 kN and 80 kN avoids joint distortion or sheet cracking caused by over-setting, while eliminating loose joints from under-setting. Proper tonnage yields uniform button head geometry across diverse material hardnesses.
Q: Can SPR tooling be used for aluminum body repairs and prototype development?
A: Absolutely. SPR systems adhere to OEM repair standards across brands like Ford (F-150), Tesla, NIO, BMW, and Porsche, delivering cold-fastening capability paired with structural adhesive bonding.
Q: What quality control measures are performed before shipping SPR systems?
A: Every system undergoes complete operational testing and force calibration. Detailed video and photo documentation are provided for customer verification prior to dispatch.
Conclusion and Engineering Support
Selecting an ideal SPR riveting system demands matching total stack thickness and joint accessibility with precise hydraulic output up to 80 kN. Supported by ODM/OBM manufacturing practices and strict pre-delivery testing, high-quality SPR systems ensure long-term process repeatability for automotive production. For customized engineering consultation, contact us at jane@questok.com.
About Our Organization
PHOTON TECHNOLOGY KUNSHAN CO.,LTD (brand Questok) is a premier industrial solution provider focused on advanced fastening, clinching, and mechanical joining technologies. Founded in 2011, Questok operates a 5,000 m² facility with a specialized R&D team carrying over a decade of hands-on application experience. Offering CE and MSDS certified SPR equipment, Questok supports automotive OEMs, EV battery innovators, and global industrial fabricators.
REPORT